

| Supply scope | Filling, capping, labelling and packing equipment |
| Sizing basis | Demand in units per day, divided by productive hours and a production factor |
| Production factor | 0.65-0.85 depending on formats and changeovers |
| Key control | Fill accuracy, closure integrity, changeover time |
| Key decision | One flexible line or two dedicated lines |
| Acceptance | Output, accuracy, closure and changeover, measured |
Settle the product and the package before the machine. Product viscosity, acidity, carbonation and particle size decide the filling principle; the bottle neck finish decides the capping head and the change parts. A machine chosen before those two are fixed is chosen twice.
Changeover, CIP, label roll changes and downstream stops. A line rated at 12,000 BPH and run with four formats and two changeovers per shift delivers closer to 8,000. The production factor is not a discount on the machine; it is what the plant actually gets.
Small, squeezable, light and cheap; PE bottle lines handle 2oz formats efficiently.
| Decision | What it fixes | What it does not fix |
|---|---|---|
| Filling principle | Product and accuracy | Downstream capacity |
| Valve count | Rated BPH | Changeover and CIP time |
| Automation level | Labour per shift | Product quality |
| Line layout | Floor space and flow | Throughput of the slowest station |
Site requirements, air and water consumption sit with the Gravity Filling Machine for Still Water.
It proves the machine meets the written specification on the agreed product, at the agreed format, in the builder workshop. It does not prove the line will run in your building. Both tests are needed, and the second one is where most disputes start.
Functional beverages—energy shots, vitamin waters, probiotic and collagen drinks, electrolyte mixes—are the fastest-growing corner of the category, projected to exceed USD 200 billion globally by 2030 at a CAGR above 8%.
Sizing for this duty runs through the Volumetric Filling Machine for Still Water, where the valve count is set out.
At 1:100, with conveyor radii, maintenance access and the largest format drawn in. Most layout problems appear as a service door that cannot open or a pallet that cannot turn. Fixing them on paper costs nothing; fixing them on site costs weeks.
The same question is worked through from another angle in Double-Head Sleeving Machine: Throughput and Film Control.
Bottles per day divided by productive hours, then divided by a production factor of 0.65-0.85. The factor covers changeover, cleaning and downstream stops. Sizing at 1.0 is the most common planning error.
BPH is bottles per hour; divide by 60 for bottles per minute. A 12,000 BPH line runs at 200 bottles per minute, and every downstream machine has to carry that rate.
Capacity is usually added by a second line or by a downstream upgrade, not by speeding up the filler. The filler, the capper and the packer are matched, so raising one alone moves the bottleneck.
Ask for the factory acceptance test procedure, a reference line running the same format, and the spare parts list with lead times. A supplier who cannot show a running line has not commissioned many.
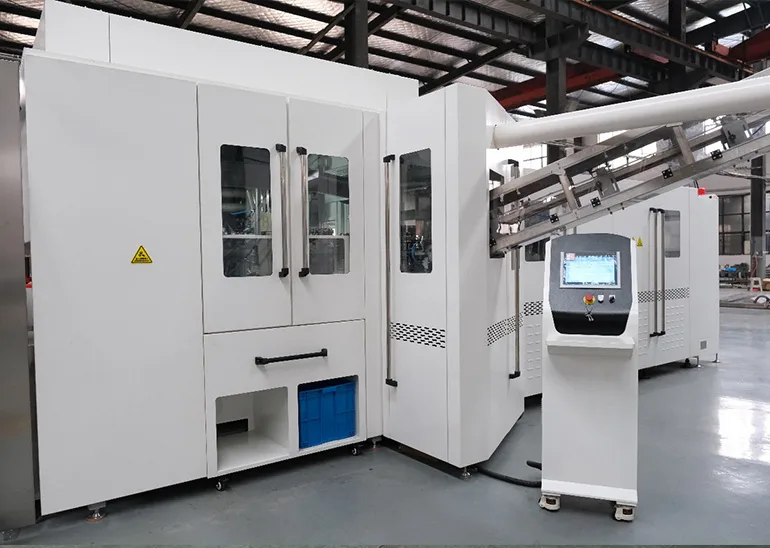
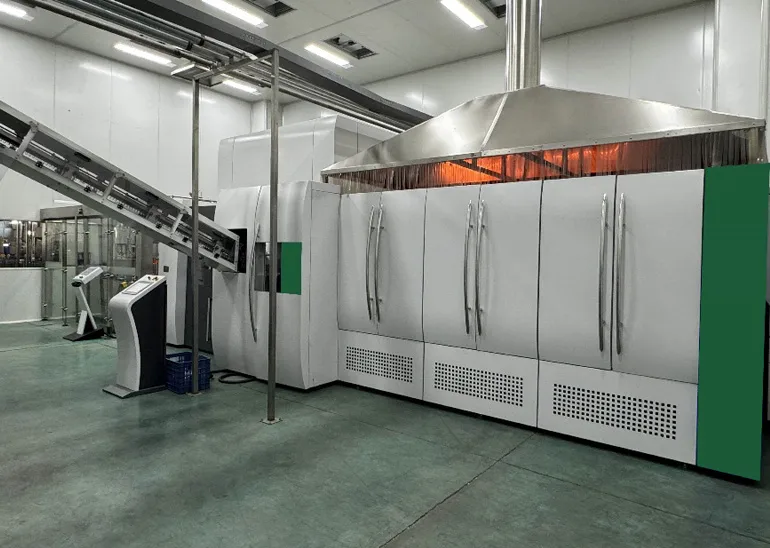
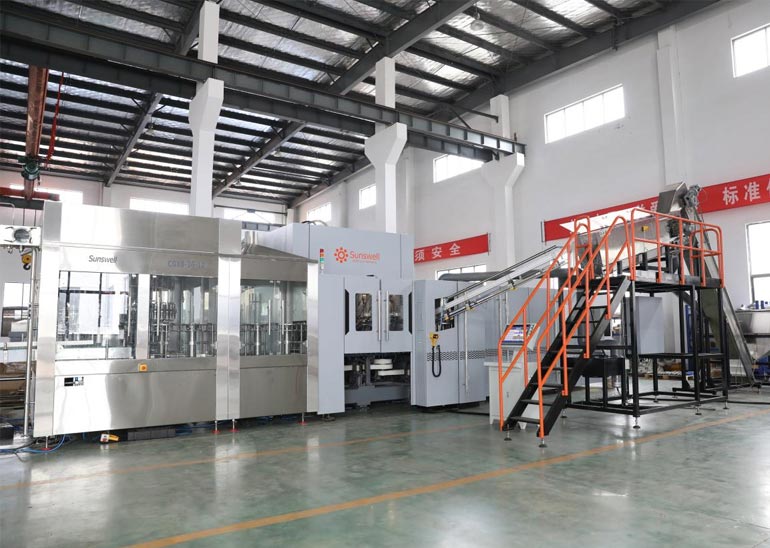
Country:Kazakhstan
Product: PET Bottled Sparkling Water, Canned Soft Drink, Canned Tea
Capacity: 25000CPH (250ml)
Solution:Three Lines,7000BPH(1.5L), 15000CPH(330ml),15000CPH(450ml)



 +86 13921964455
 [email protected]

A2 Dongjiu Industrial Park, 30 East Jintang Road, Tangshi, Zhangjiagang, Jiangsu 215600, China


