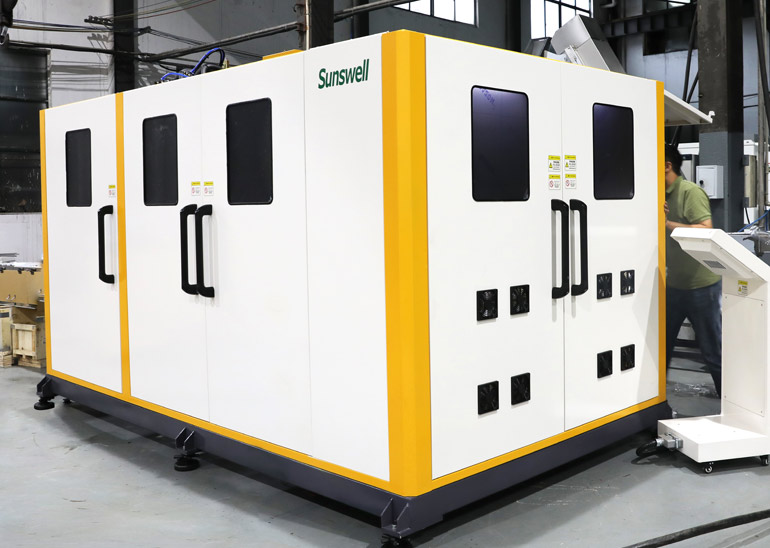
| Types | Linear and rotary blow moulding |
| Input | PET preform, heated in an oven before blowing |
| Output | Bottle matched to the filler neck and format |
| Key control | Preform temperature profile, mould cooling, stretch ratio |
| Integration | Stand-alone, or inside a combiblock |
| Key decision | Blow in-house or buy bottles |
A mould change is a mechanical operation: mould halves, bottom insert, stretch rod height, oven recipe and gripper settings. On a linear machine it is a scheduled stop measured in tens of minutes; on a rotary machine it is longer because there are more cavities to set.
Blowing needs high-pressure air, and producing it is the largest single energy cost in a PET line. Recovery of blowing air, correct nozzle sizing and leak maintenance on the high-pressure circuit are the three measures that move the number, and none of them is visible in a machine quotation.
| Machine | Output pattern | Format changes |
|---|---|---|
| Linear | Lower output, more formats | Frequent, shorter changeover |
| Rotary | High output, fewer formats | Longer changeover, more cavities |
| Two-stage on site | Preform bought in | Mould per format still required |
| Combiblock integrated | Linked to filler | Changeover stops the whole block |
Rated output, change parts and services are listed on the Linear Blow Molding page.
Neck finish decides the filler and capper change parts. Body shape decides the star wheels and guide rails. Wall thickness decides whether the bottle survives the filler and the conveyor. A lightweighting project that changes the base is a filling line project as much as a bottle project.
The specification sheet for the Rotary Blow Molding carries the utility figures quoted here.
Zone by zone along the preform, with more heat at the body and less at the neck. The profile follows the preform geometry and the bottle design. It is set once and checked on a schedule, because lamp ageing shifts it slowly.
The same question is worked through from another angle in PET Bottle Blowing Machines: Integration with Your Water Filling.
A linear machine moves preforms through heating and blowing in a straight path and suits lower outputs and frequent format changes. A rotary machine carries moulds on a wheel and suits high output with fewer changeovers.
One preform per bottle. The preform weight is the bottle weight, so preform lightweighting is the main material saving, and it changes the blowing recipe and often the mould.
Indirectly. Wall thickness distribution and base quality decide the bottle's mechanical strength and its barrier performance. A bottle that passes the drop test can still lose carbonation if the wall is thin at the base.
It is a scheduled stop measured in tens of minutes on a linear machine and longer on a rotary machine, because every cavity is set. The oven recipe and the stretch rod height change with the mould.
Country:Kazakhstan
Product: PET Bottled Sparkling Water, Canned Soft Drink, Canned Tea
Capacity: 25000CPH (250ml)
Solution:Three Lines,7000BPH(1.5L), 15000CPH(330ml),15000CPH(450ml)



 +86 13921964455
 [email protected]

A2 Dongjiu Industrial Park, 30 East Jintang Road, Tangshi, Zhangjiagang, Jiangsu 215600, China