| Scope | Filling, capping, labelling and packing equipment |
| Sizing basis | Demand in units per day, divided by productive hours and a production factor |
| Production factor | 0.65-0.85 depending on formats and changeovers |
| Key control | Fill accuracy, closure integrity, changeover time |
| Key decision | One flexible line or two dedicated lines |
| Acceptance | Output, accuracy, closure and changeover, measured |
Settle the product and the package before the machine. Product viscosity, acidity, carbonation and particle size decide the filling principle; the bottle neck finish decides the capping head and the change parts. A machine chosen before those two are fixed is chosen twice.
It proves the machine meets the written specification on the agreed product, at the agreed format, in the builder workshop. It does not prove the line will run in your building. Both tests are needed, and the second one is where most disputes start.
| Decision | What it fixes | What it does not fix |
|---|---|---|
| Filling principle | Product and accuracy | Downstream capacity |
| Valve count | Rated BPH | Changeover and CIP time |
| Automation level | Labour per shift | Product quality |
| Line layout | Floor space and flow | Throughput of the slowest station |
Valve count, utility schedule and footprint sit on the Gravity Filling Machine for Still Water page.
At 1:100, with conveyor radii, maintenance access and the largest format drawn in. Most layout problems appear as a service door that cannot open or a pallet that cannot turn. Fixing them on paper costs nothing; fixing them on site costs weeks.
Where this becomes a line rather than a single machine, the Volumetric Filling Machine for Still Water is the starting point.
Capacity is what the machine can do at steady state in one format. Throughput is what the plant gets across a week of changeovers, cleaning and stops. Plans built on capacity alone are the reason new lines look slow in their first month.
The same question is worked through from another angle in Filling precision analysis of high tank.
Bottles per day divided by productive hours, then divided by a production factor of 0.65-0.85. The factor covers changeover, cleaning and downstream stops. Sizing at 1.0 is the most common planning error.
BPH is bottles per hour; divide by 60 for bottles per minute. A 12,000 BPH line runs at 200 bottles per minute, and every downstream machine has to carry that rate.
Capacity is usually added by a second line or by a downstream upgrade, not by speeding up the filler. The filler, the capper and the packer are matched, so raising one alone moves the bottleneck.
Between 0.65 and 0.85. A single-format line on one shift sits near 0.85; a line with four formats and two changeovers per shift sits near 0.65.
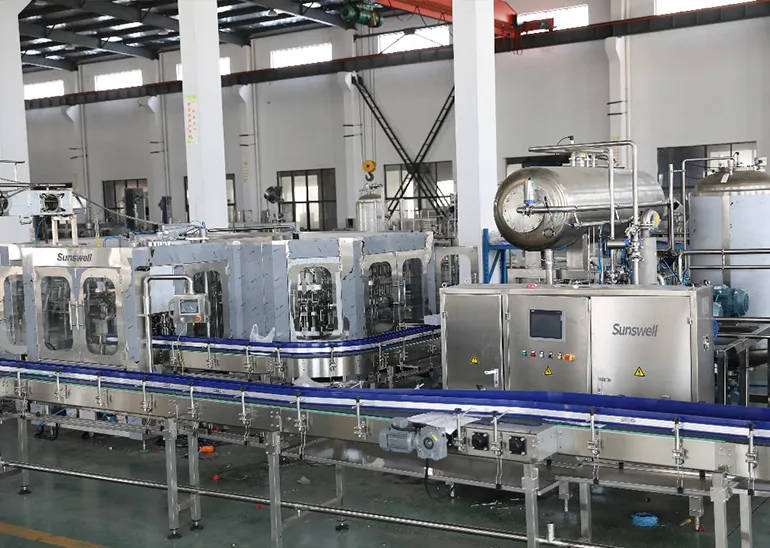
Country:Kazakhstan
Product: PET Bottled Sparkling Water, Canned Soft Drink, Canned Tea
Capacity: 25000CPH (250ml)
Solution:Three Lines,7000BPH(1.5L), 15000CPH(330ml),15000CPH(450ml)


 +86 13921964455
 [email protected]

A2 Dongjiu Industrial Park, 30 East Jintang Road, Tangshi, Zhangjiagang, Jiangsu 215600, China


