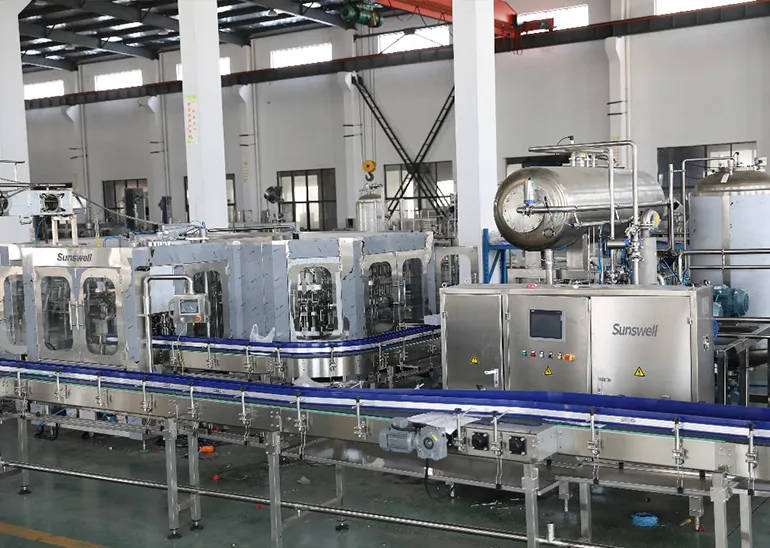
| What is included | Printers, coders, cap feeders, nitrogen dosers, detectors |
| Function | Support the filler without changing its rating |
| Key control | Position, timing, consumable cost |
| Integration | Signals from the filler PLC or a standalone sensor |
| Key decision | Whether the device earns its cost per 1,000 units |
| Typical position | After the filler, before the packer |
Position follows the signal. A coder needs the bottle presented at a fixed gap; a cap feeder needs a buffer before the capper; a detector needs a clear view and a reject gate downstream. Moving any of them changes the timing and the reject logic.
Ink, solvent, laser power, nitrogen, caps and labels all carry a per-unit cost that does not appear in the machine price. A device with a low purchase price and a high consumable cost can be the most expensive item on the line over five years.
| Device | What it controls | Consumable |
|---|---|---|
| Coder or printer | Date and batch code | Ink, solvent or laser power |
| Cap feeder | Cap supply to the capper | None, but a buffer is needed |
| Nitrogen doser | Headspace oxygen | Nitrogen per 1,000 units |
| Fill level detector | Reject decision | None, but a reject gate is needed |
Site requirements, air and power consumption sit with the Accessory.
Either through a discrete signal from the filler PLC, which is simple and reliable, or through the line network, which allows recipes and reporting. Discrete signals are easier to commission; network integration is easier to audit. Choose based on who will maintain it.
Site requirements, air and power consumption sit with the Conveying.
Run the device at the line rating, not at a demonstration speed, and count rejects with the device on and off. Acceptance at half speed hides the timing problem that appears in the first production week.
The same question is worked through from another angle in Blow Mould Quality: What a Buyer Should Check.
Through an encoder on the conveyor, so the print position follows the actual speed rather than a set value. Without the encoder, the code stretches when the line accelerates and lands off-centre.
Yes, with a reject gate and a shift register that tracks the bottle from the sensor to the gate. Without the register, the gate rejects the wrong bottle.
A laser marks the surface and needs no consumable ink, but it needs a clear line of sight and a consistent bottle position. An inkjet prints on most surfaces and carries ink and solvent cost.
Caps arrive out of orientation, the elevator runs faster than the chute can release, or the chute angle is wrong for the cap. Most jams are a chute and speed setting, not a cap defect.
Yes. Detection without a reject gate only records the defect. The gate needs a shift register so it rejects the bottle that was measured, not the one behind it.
Between the filler and the closure, close enough that the gas stays in the headspace. Moving it further downstream wastes gas and gives an unstable result.
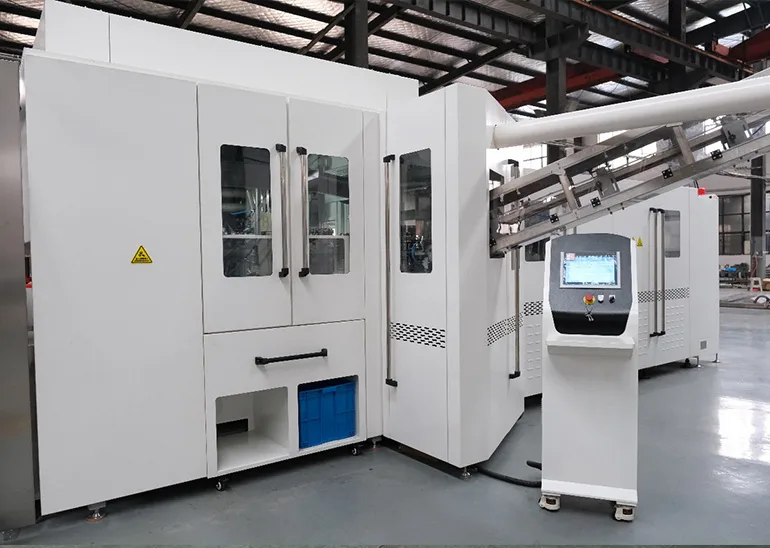
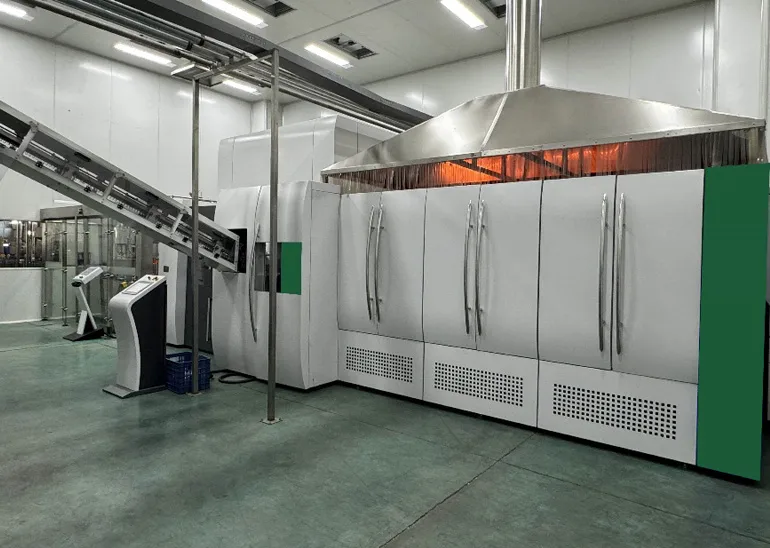
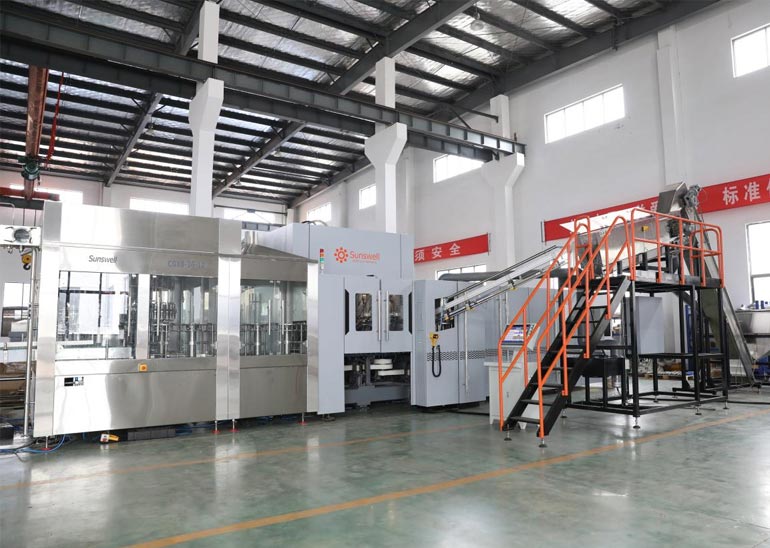
Country:Kazakhstan
Product: PET Bottled Sparkling Water, Canned Soft Drink, Canned Tea
Capacity: 25000CPH (250ml)
Solution:Three Lines,7000BPH(1.5L), 15000CPH(330ml),15000CPH(450ml)



 +86 13921964455
 [email protected]

A2 Dongjiu Industrial Park, 30 East Jintang Road, Tangshi, Zhangjiagang, Jiangsu 215600, China