

| Scope | Filling, capping, labelling and packing equipment |
| Sizing basis | Demand in units per day, divided by productive hours and a production factor |
| Production factor | 0.65-0.85 depending on formats and changeovers |
| Key control | Fill accuracy, closure integrity, changeover time |
| Key decision | One flexible line or two dedicated lines |
| Acceptance | Output, accuracy, closure and changeover, measured |
Settle the product and the package before the machine. Product viscosity, acidity, carbonation and particle size decide the filling principle; the bottle neck finish decides the capping head and the change parts. A machine chosen before those two are fixed is chosen twice.
Compare the lowest rated station, the changeover time, the CIP time and the consumable cost per 1,000 units. A lower price with a slower packer or a longer CIP is not a lower cost. Ask both suppliers for the same four numbers in writing.
| Decision | What it fixes | What it does not fix |
|---|---|---|
| Filling principle | Product and accuracy | Downstream capacity |
| Valve count | Rated BPH | Changeover and CIP time |
| Automation level | Labour per shift | Product quality |
| Line layout | Floor space and flow | Throughput of the slowest station |
Site requirements, air and water consumption sit with the Gravity Filling Machine for Still Water.
Changeover, CIP, label roll changes and downstream stops. A line rated at 12,000 BPH and run with four formats and two changeovers per shift delivers closer to 8,000. The production factor is not a discount on the machine; it is what the plant actually gets.
A different bottle format means a different unit; see the Volumetric Filling Machine for Still Water.
When the formats are far apart, or when one product cannot tolerate the cleaning regime of the other. A single flexible line carries changeover cost every day; two dedicated lines carry capital cost once. The crossover is usually visible in the annual changeover hours.
The same question is worked through from another angle in GULFOOD Manufacturing: What We Showed.
Bottles per day divided by productive hours, then divided by a production factor of 0.65-0.85. The factor covers changeover, cleaning and downstream stops. Sizing at 1.0 is the most common planning error.
BPH is bottles per hour; divide by 60 for bottles per minute. A 12,000 BPH line runs at 200 bottles per minute, and every downstream machine has to carry that rate.
A monoblock combines rinse, fill and cap on one frame. A full line adds treatment, blowing, labelling, packing and palletizing around it. The monoblock is one station in a longer chain.
Between 0.65 and 0.85. A single-format line on one shift sits near 0.85; a line with four formats and two changeovers per shift sits near 0.65.


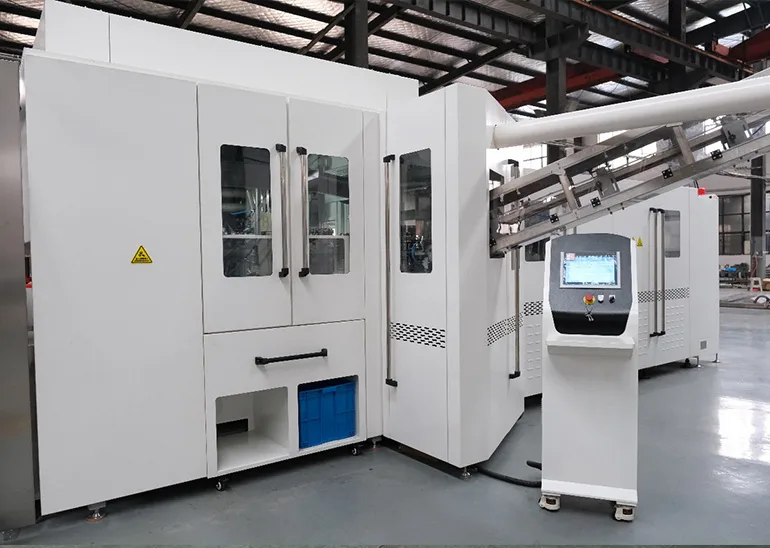
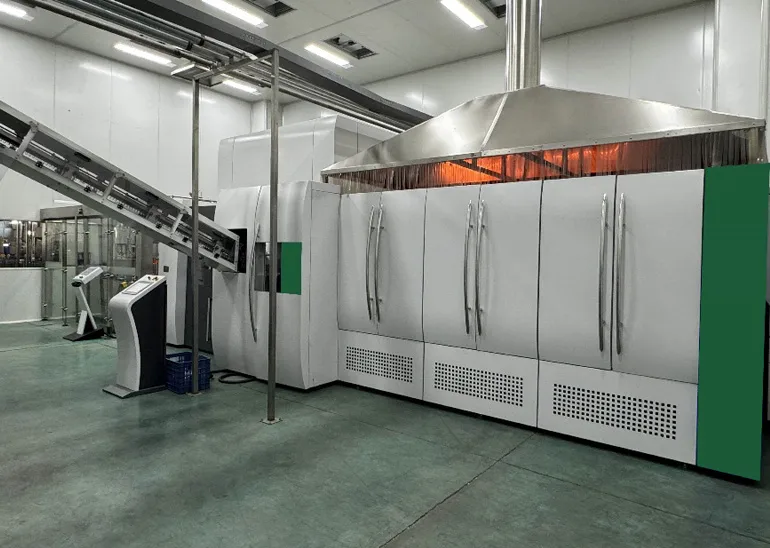
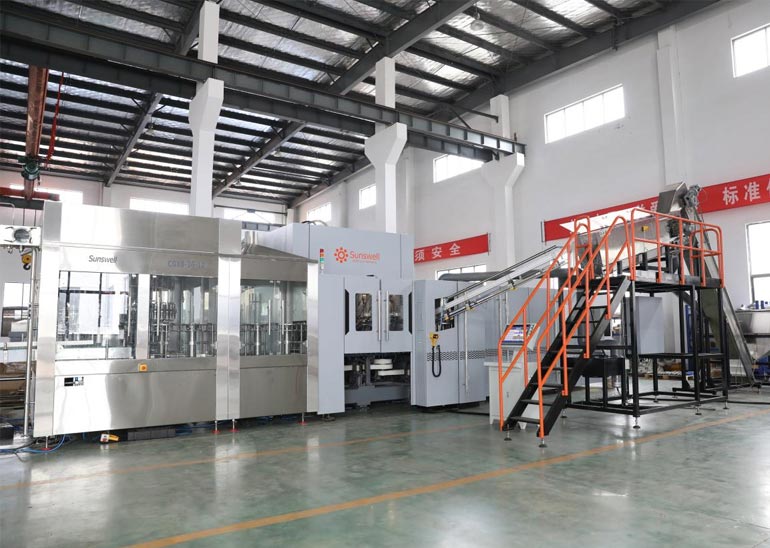
Country:Kazakhstan
Product: PET Bottled Sparkling Water, Canned Soft Drink, Canned Tea
Capacity: 25000CPH (250ml)
Solution:Three Lines,7000BPH(1.5L), 15000CPH(330ml),15000CPH(450ml)



 +86 13921964455
 [email protected]

A2 Dongjiu Industrial Park, 30 East Jintang Road, Tangshi, Zhangjiagang, Jiangsu 215600, China


