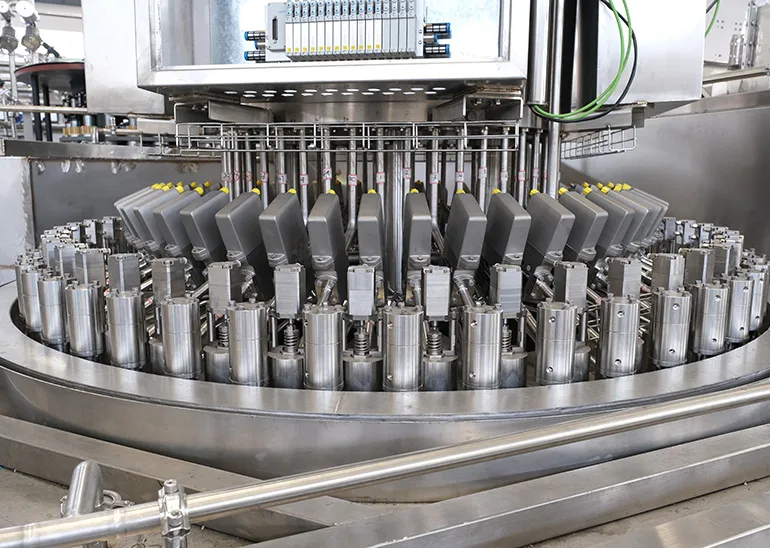
| Filling method | Hot-fill, up to 85 C |
| Output range | 6,000-36,000 BPH at 0.2-2 L |
| Container | Heat-resistant PET geometry, or glass |
| Line | Hot-fill monobloc with tunnel pasteuriser |
| Products | Juice, tea, nectar, functional drinks |
| Key control | Fill temperature, hold time, cap seal |
Maintenance effort should follow the wear map, not the machine layout. Seals, capping inserts, guide rail blocks and filters account for most unplanned stops; painting and polishing account for none. A short daily check on those four items beats a long monthly inspection.
Pulp needs either a larger valve bore or a piston filler, and it needs continuous gentle agitation in the bowl. Dead corners in the product path settle fibre, then release it as a slug into the next bottle. Bowl geometry and return-flow design matter more than valve count here.
| Route | Temperature | What it costs |
|---|---|---|
| Hot fill | Up to 85 C | Heat-resistant bottle and a cooling tunnel |
| Cold fill with preservative | Ambient | Formulation constraint, not a machine constraint |
| Cold fill with in-line pasteuriser | Product-side only | Separate pasteuriser and a closed filling zone |
| Hot fill in glass | Up to 85 C | Glass mass, slower line, higher transport cost |
Site requirements, air and water consumption sit with the Juice By Volumetric Filler.
Cap seals and filling valve O-rings, because they see the highest temperature every cycle. A seal that is fine on a water line at 20 C will harden in weeks at 85 C. The spare parts list should carry those two items in proportion to the number of valves, not as a single set.
Valve count, utility schedule and footprint sit on the Hotfill Type Filling Machine for Juice page.
Glass brings mass, breakage and a slower line. It also brings a closure decision: crown, lug or screw. A glass hot-fill line usually runs at a lower rate than the same filler on PET, and the difference is handling and inspection, not the valve.
The same question is worked through from another angle in Best Practices for Hotfill Juice Production Lines.
No. Standard PET softens and deforms at fill temperature. The bottle needs a heat-resistant geometry, and the mould and preform are part of the project, not an afterthought.
Usually fill temperature above the bottle rating, or a vacuum that forms as the product cools. Check the fill temperature against the bottle specification and the cap seal before changing the cooling profile.
Heat-sensitive pigments and vitamins degrade above the product temperature limit. The fill temperature and the hold time are the two variables; lowering either protects colour and shortens the microbial margin.
A controlled ramp rather than a cold plunge, so the bottle does not deform under vacuum. The tunnel zones are set per bottle geometry and validated with a temperature probe in the product.
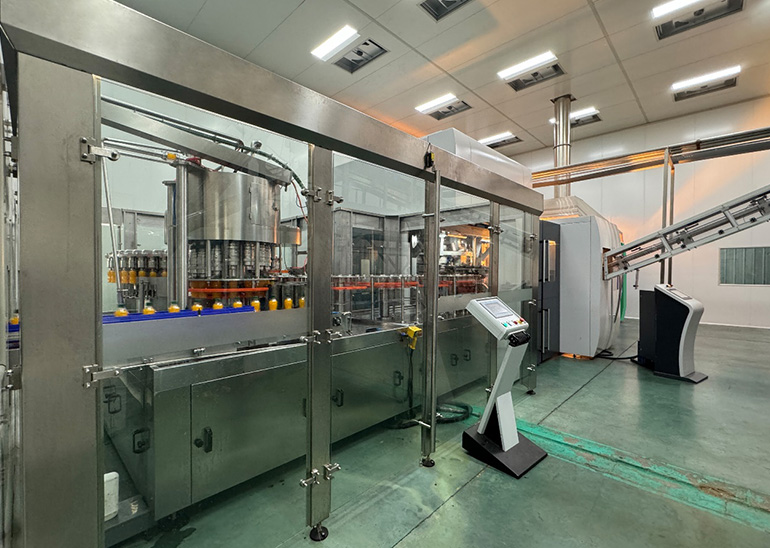
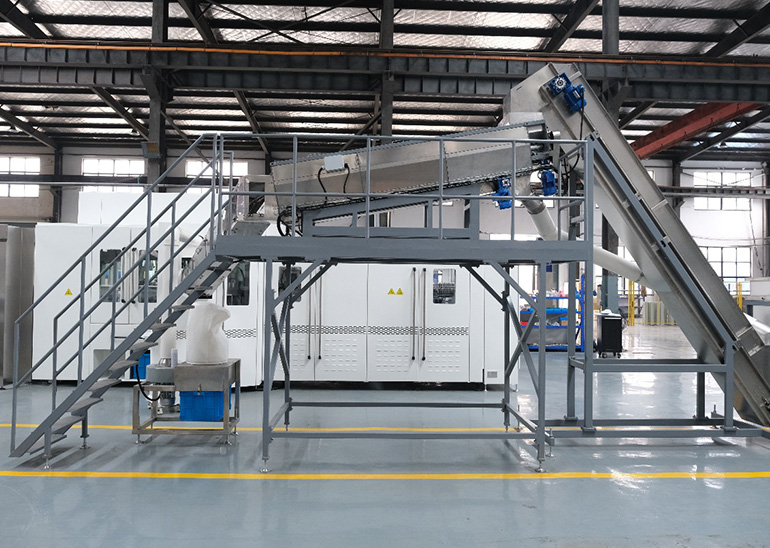
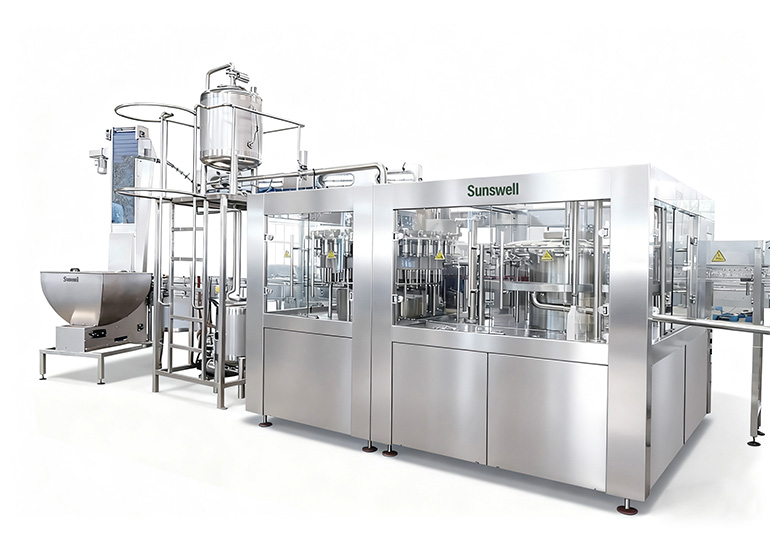
Country: Turkey
Product: Glass and PET Bottled Juice
Capacity: 20000BPH(330ml) Glass Bottle; 4000BPH(3L) PET Bottle
Solution:Juice Production Line
Country:Kazakhstan
Product: PET Bottled Sparkling Water, Canned Soft Drink, Canned Tea
Capacity: 25000CPH (250ml)
Solution:Three Lines,7000BPH(1.5L), 15000CPH(330ml),15000CPH(450ml)



 +86 13921964455
 [email protected]

A2 Dongjiu Industrial Park, 30 East Jintang Road, Tangshi, Zhangjiagang, Jiangsu 215600, China