
| What is included | Filling, capping and closing equipment |
| Filling principles | Gravity, volumetric, isobaric, piston, load cell |
| Output range | 2,000-48,000 BPH by configuration |
| Accuracy basis | Volume, weight or fill level |
| Wetted parts | SUS 304 product contact, CIP-ready |
| Key control | Fill accuracy, closure integrity, CIP time |
Four variables sit behind a fill number: the dosing principle, the product temperature, the bottle geometry, and the condition of the valve or piston seal. A machine that holds its tolerance on the factory test can drift in the plant when the product arrives warmer or the bottle wall gets thinner.
Rated output at the specified format, fill accuracy on a defined sample, closure torque or seal measurement, and a timed changeover with the buyer watching. Anything not measured before sign-off becomes a discussion after the final payment.
| Principle | Doses by | Fails when |
|---|---|---|
| Gravity | Fill level in the bottle | Bottle geometry varies |
| Volumetric | Chamber volume | Valve seal wears |
| Isobaric | Volume under counter-pressure | Pressure or temperature drifts |
| Piston | Displacement | Product carries solids |
| Load cell | Net weight | Product temperature moves |
Site requirements, air and water consumption sit with the Gravity Filling Machine for Still Water.
Valve count follows the target BPH and the fill time per valve. Longer fill time, thicker product or a taller bottle all reduce the rate per valve, so the same BPH needs more valves. Buying valves for a water duty and running juice on them is a common and expensive mismatch.
A different bottle format means a different unit; see the Volumetric Filling Machine for Still Water.
The parts cost is small; the time is not. A format change touches star wheels, guide rails, grippers, the cap chute and the recipe. On a line with two formats and two changes a day, the annual hours lost exceed the price of a second small machine in many plants.
The same question is worked through from another angle in Implementing MES on a Beverage Filling Line: Start Small.
Wiring and pneumatic diagrams, the spare parts list with lead times, the changeover checklist, the CIP recipe and the acceptance record. A line handed over without those five is a line that depends on the engineer who installed it.
It depends on the principle and the product. A volumetric or load cell filler holds a tighter band than gravity on a variable bottle. The tolerance belongs in the acceptance protocol, measured by weight on a defined sample.
Yes, with change parts: star wheels, guide rails, grippers and a recipe. The parts are cheap compared with the changeover time, which is why most plants specify one dominant format.
From tens of minutes to over an hour, set by the circuit volume and the soil. It is a fixed cost per production day and should be planned as downtime, not squeezed into the shift.
Bottle capacity variation, product temperature, valve wear or foam. On glass, mould-to-mould capacity variation alone is enough to make level filling inconsistent, which is why glass lines often check-weigh.
Valve seals, piston seals, capping head inserts, guide rail blocks and one set of change parts for the second format. These are the items that stop a line for days when they fail.
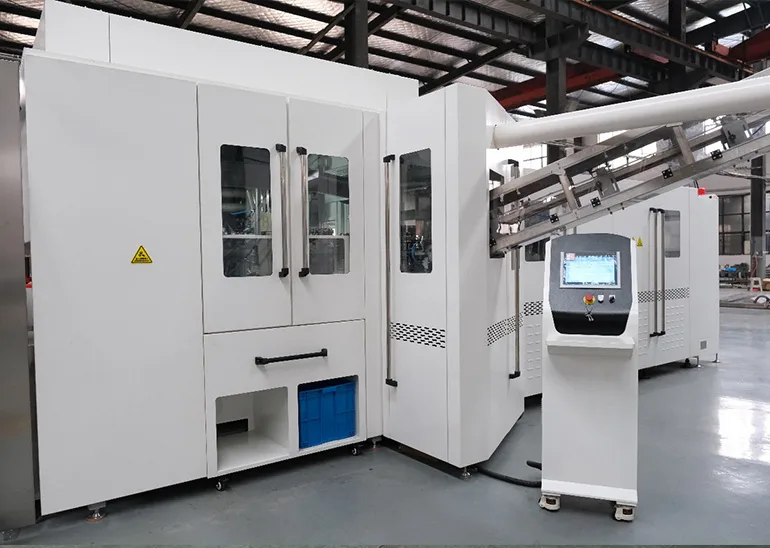
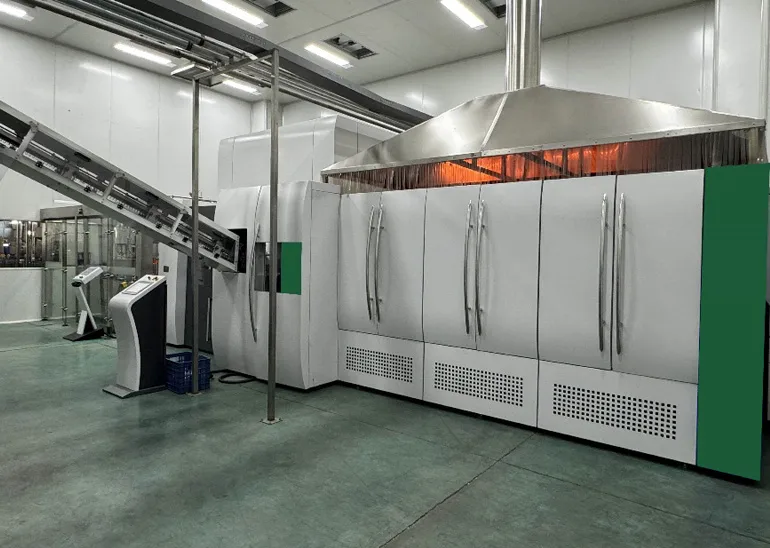
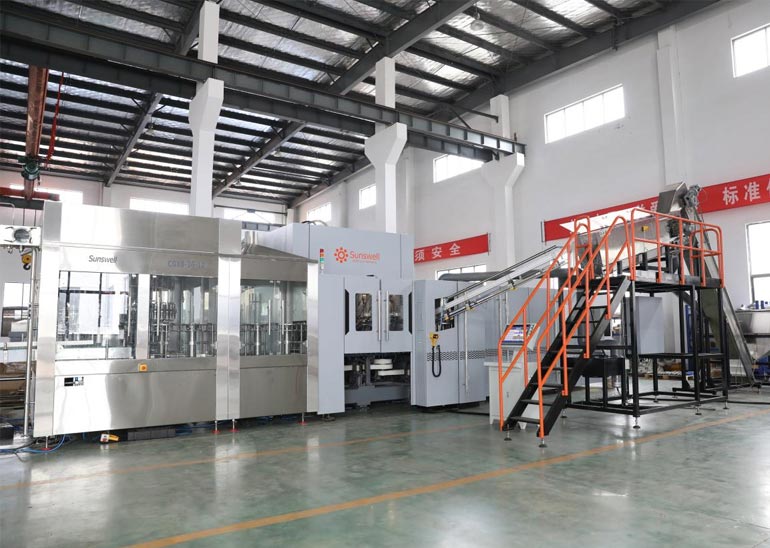
Country:Kazakhstan
Product: PET Bottled Sparkling Water, Canned Soft Drink, Canned Tea
Capacity: 25000CPH (250ml)
Solution:Three Lines,7000BPH(1.5L), 15000CPH(330ml),15000CPH(450ml)



 +86 13921964455
 [email protected]

A2 Dongjiu Industrial Park, 30 East Jintang Road, Tangshi, Zhangjiagang, Jiangsu 215600, China


