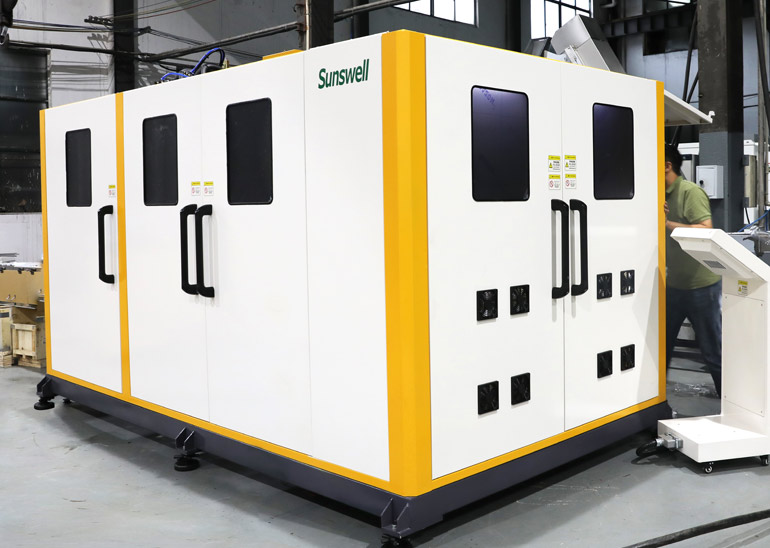
| Types | Linear and rotary blow moulding |
| Input | PET preform, heated in an oven before blowing |
| Output | Bottle matched to the filler neck and format |
| Key control | Preform temperature profile, mould cooling, stretch ratio |
| Integration | Stand-alone, or inside a combiblock |
| Key decision | Blow in-house or buy bottles |
The preform temperature profile decides where the material goes. Too cold and the base is thin; too hot and the wall stretches unevenly. The mould cools the bottle into shape, and the stretch ratio set by the rod and the mould height fixes the wall distribution.
One practical approach to enhancing wall thickness is through the manipulation of process parameters such as air pressure, mold temperature, and cooling rate.
A mould change is a mechanical operation: mould halves, bottom insert, stretch rod height, oven recipe and gripper settings. On a linear machine it is a scheduled stop measured in tens of minutes; on a rotary machine it is longer because there are more cavities to set.
| Machine | Output pattern | Format changes |
|---|---|---|
| Linear | Lower output, more formats | Frequent, shorter changeover |
| Rotary | High output, fewer formats | Longer changeover, more cavities |
| Two-stage on site | Preform bought in | Mould per format still required |
| Combiblock integrated | Linked to filler | Changeover stops the whole block |
Site requirements, air and water consumption sit with the Linear Blow Molding.
Blowing needs high-pressure air, and producing it is the largest single energy cost in a PET line. Recovery of blowing air, correct nozzle sizing and leak maintenance on the high-pressure circuit are the three measures that move the number, and none of them is visible in a machine quotation.
The specification sheet for the Rotary Blow Molding carries the utility figures quoted here.
Neck finish decides the filler and capper change parts. Body shape decides the star wheels and guide rails. Wall thickness decides whether the bottle survives the filler and the conveyor. A lightweighting project that changes the base is a filling line project as much as a bottle project.
By strategically designing the bottle's contours and reinforcing key stress points, manufacturers can significantly improve its resistance to pressure, impact, and environmental factors.
The same question is worked through from another angle in 12,000 BPH Dual-Cavity PET Blow Moulding Line.
A linear machine moves preforms through heating and blowing in a straight path and suits lower outputs and frequent format changes. A rotary machine carries moulds on a wheel and suits high output with fewer changeovers.
One preform per bottle. The preform weight is the bottle weight, so preform lightweighting is the main material saving, and it changes the blowing recipe and often the mould.
It follows the bottle design and the shelf life requirement, and it is set with the preform supplier. Lighter preforms save material and reduce the process window, so the blowing recipe has to be re-validated.
It can, with an adjusted temperature profile, because recycled resin melts and stretches differently. The change is a process change, and it should be validated on the actual resin before production.
Country:Kazakhstan
Product: PET Bottled Sparkling Water, Canned Soft Drink, Canned Tea
Capacity: 25000CPH (250ml)
Solution:Three Lines,7000BPH(1.5L), 15000CPH(330ml),15000CPH(450ml)



 +86 13921964455
 [email protected]

A2 Dongjiu Industrial Park, 30 East Jintang Road, Tangshi, Zhangjiagang, Jiangsu 215600, China