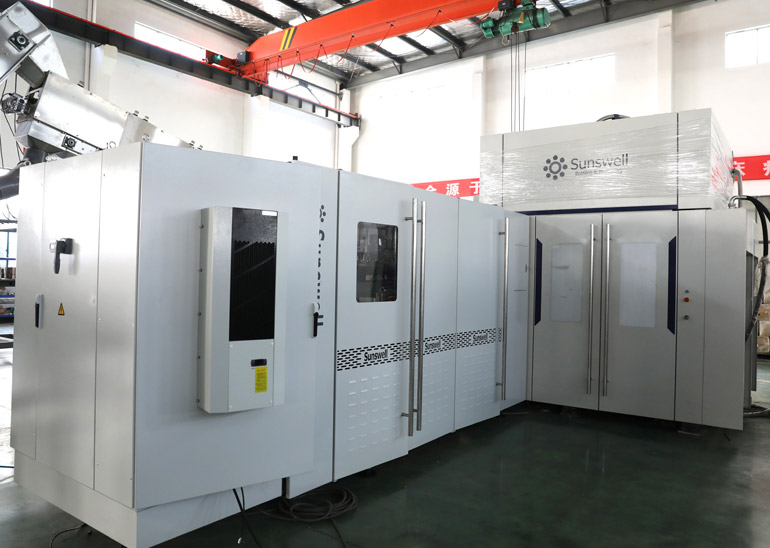
| Scope | Filling, capping and closing equipment |
| Filling principles | Gravity, volumetric, isobaric, piston, load cell |
| Capacity | 2,000-48,000 BPH by configuration |
| Accuracy basis | Volume, weight or fill level |
| Material | SUS 304 product contact, CIP-ready |
| Key control | Fill accuracy, closure integrity, CIP time |
A CIP cycle is measured in tens of minutes to over an hour depending on the circuit and the soil. It is not production time, and a plan that counts it as production will miss its daily output every day. The number belongs in the capacity calculation, not in the shift handover.
Foaming product needs a slower fill ramp and often a longer nozzle that reaches below the surface. The machine is the same frame with a different valve and a different cam or recipe. Sizing it on the water rate and hoping the foam settles is how lines end up at half output.
| Principle | Doses by | Fails when |
|---|---|---|
| Gravity | Fill level in the bottle | Bottle geometry varies |
| Volumetric | Chamber volume | Valve seal wears |
| Isobaric | Volume under counter-pressure | Pressure or temperature drifts |
| Piston | Displacement | Product carries solids |
| Load cell | Net weight | Product temperature moves |
For the same duty in another bottle format, the Gravity Filling Machine for Still Water is specified separately.
It saves capital and floor space, and it costs labour per shift. Manual loading, manual packing and manual palletizing are the usual trades. For a small plant with a single format and a flexible crew, that is a sensible trade; for a plant running three shifts it is not.
The Volumetric Filling Machine for Still Water is the reference unit for this configuration.
When the formats are far apart or the cleaning regimes conflict. Two smaller fillers each run at their own rate and can be cleaned independently. One large flexible filler carries every changeover on the critical path, and its downtime is the plant downtime.
The same question is worked through from another angle in How Automation Reduces Error Rates in Filling Lines.
Gravity fills to a level set by a tube, so accuracy depends on the bottle. Because volumetric filling doses by chamber volume, accuracy holds across bottle sizes. Gravity is simpler and cheaper; volumetric is more repeatable when the bottle changes.
Yes, with change parts: star wheels, guide rails, grippers and a recipe. The parts are cheap compared with the changeover time, which is why most plants specify one dominant format.
A single frame carrying the rinser, the filler and the capper, driven and controlled together. It removes two transfers and the floor space between three separate machines.
Bottle capacity variation, product temperature, valve wear or foam. On glass, mould-to-mould capacity variation alone is enough to make level filling inconsistent, which is why glass lines often check-weigh.
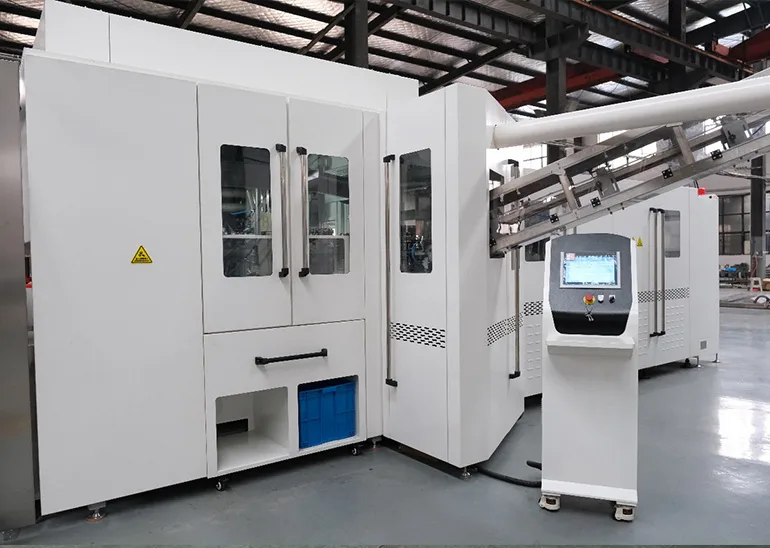
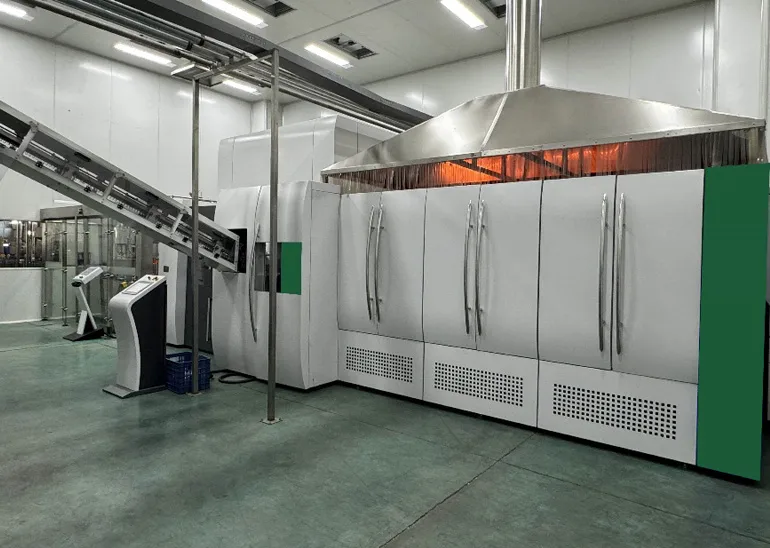
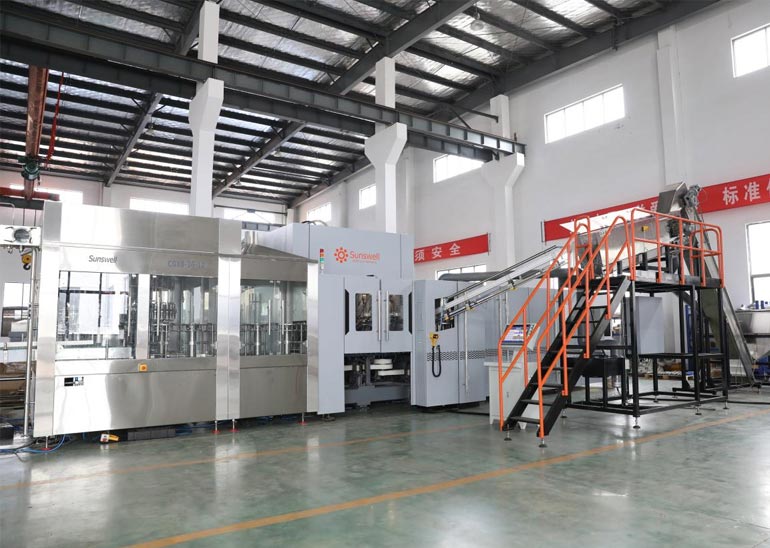
Country:Kazakhstan
Product: PET Bottled Sparkling Water, Canned Soft Drink, Canned Tea
Capacity: 25000CPH (250ml)
Solution:Three Lines,7000BPH(1.5L), 15000CPH(330ml),15000CPH(450ml)



 +86 13921964455
 [email protected]

A2 Dongjiu Industrial Park, 30 East Jintang Road, Tangshi, Zhangjiagang, Jiangsu 215600, China