
| What is included | Filling, capping, labelling and packing equipment |
| Sizing basis | Demand in units per day, divided by productive hours and a production factor |
| Production factor | 0.65-0.85 depending on formats and changeovers |
| Key control | Fill accuracy, closure integrity, changeover time |
| Key decision | One flexible line or two dedicated lines |
| Acceptance | Output, accuracy, closure and changeover, measured |
Settle the product and the package before the machine. Product viscosity, acidity, carbonation and particle size decide the filling principle; the bottle neck finish decides the capping head and the change parts. A machine chosen before those two are fixed is chosen twice.
Compare the lowest rated station, the changeover time, the CIP time and the consumable cost per 1,000 units. A lower price with a slower packer or a longer CIP is not a lower cost. Ask both suppliers for the same four numbers in writing.
| Decision | What it fixes | What it does not fix |
|---|---|---|
| Filling principle | Product and accuracy | Downstream capacity |
| Valve count | Rated BPH | Changeover and CIP time |
| Automation level | Labour per shift | Product quality |
| Line layout | Floor space and flow | Throughput of the slowest station |
The Gravity Filling Machine for Still Water is the matching unit when this becomes a line project.
Changeover, CIP, label roll changes and downstream stops. A line rated at 12,000 BPH and run with four formats and two changeovers per shift delivers closer to 8,000. The production factor is not a discount on the machine; it is what the plant actually gets.
For the same duty in another bottle format, the Volumetric Filling Machine for Still Water is specified separately.
When the formats are far apart, or when one product cannot tolerate the cleaning regime of the other. A single flexible line carries changeover cost every day; two dedicated lines carry capital cost once. The crossover is usually visible in the annual changeover hours.
The same question is worked through from another angle in How Automation Reduces Labor Costs in Beverage Production.
Bottles per day divided by productive hours, then divided by a production factor of 0.65-0.85. The factor covers changeover, cleaning and downstream stops. Sizing at 1.0 is the most common planning error.
A well-maintained stainless line runs for well over a decade, with wear parts replaced on condition. The variables are water quality, cleaning regime and whether spare parts are kept in stock.
A monoblock combines rinse, fill and cap on one frame. A full line adds treatment, blowing, labelling, packing and palletizing around it. The monoblock is one station in a longer chain.
Between 0.65 and 0.85. A single-format line on one shift sits near 0.85; a line with four formats and two changeovers per shift sits near 0.65.


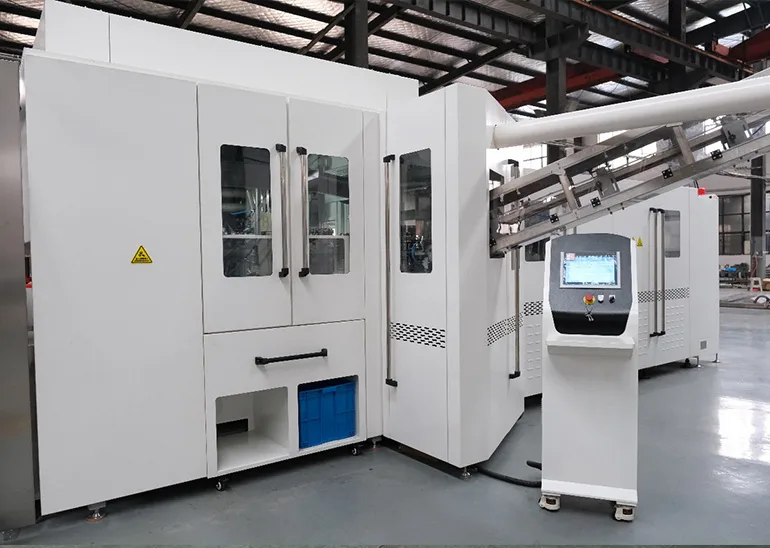
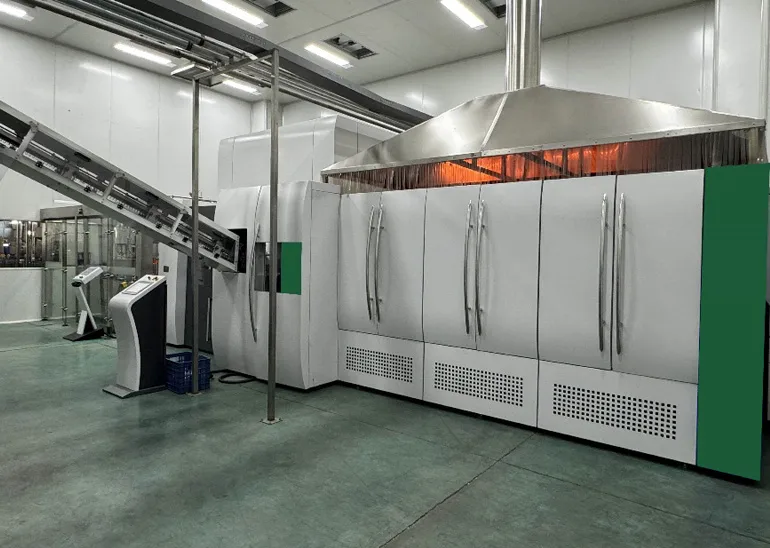
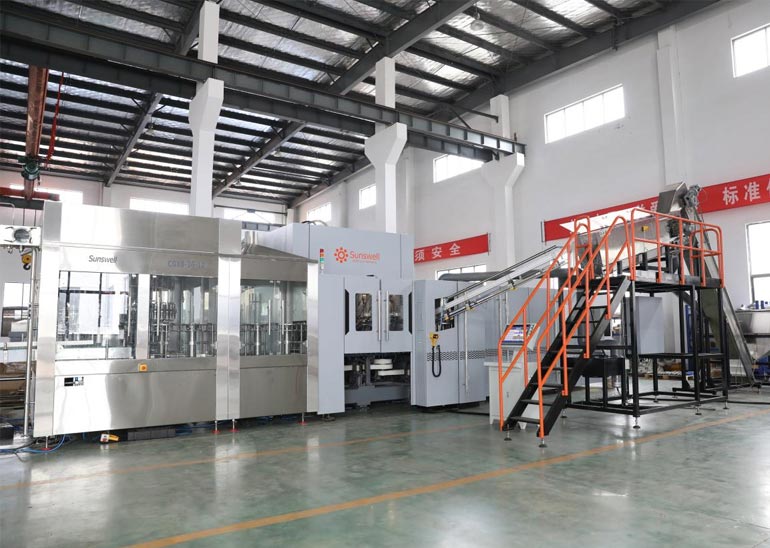
Country:Kazakhstan
Product: PET Bottled Sparkling Water, Canned Soft Drink, Canned Tea
Capacity: 25000CPH (250ml)
Solution:Three Lines,7000BPH(1.5L), 15000CPH(330ml),15000CPH(450ml)


 +86 13921964455
 [email protected]

A2 Dongjiu Industrial Park, 30 East Jintang Road, Tangshi, Zhangjiagang, Jiangsu 215600, China


