
| Supply scope | Filling, capping and closing equipment |
| Filling principles | Gravity, volumetric, isobaric, piston, load cell |
| Capacity | 2,000-48,000 BPH by configuration |
| Accuracy basis | Volume, weight or fill level |
| Contact material | SUS 304 product contact, CIP-ready |
| Key control | Fill accuracy, closure integrity, CIP time |
Filling principle comes from the product, not from the target BPH. Still liquid at a steady density runs gravity or volumetric; carbonated product needs isobaric; thick product with solids needs a piston; product sold by weight runs a load cell. A machine picked ahead of the product usually gets picked again.
As managers and decision-makers in this industry, understanding the impact of liquid viscosity on filling accuracy and speed is paramount to ensuring efficiency and product quality.
Four variables sit behind a fill number: the dosing principle, the product temperature, the bottle geometry, and the condition of the valve or piston seal. A machine that holds its tolerance on the factory test can drift in the plant when the product arrives warmer or the bottle wall gets thinner.
The viscosity of a beverage directly impacts the filling process, affecting accuracy and speed.
| Principle | Doses by | Fails when |
|---|---|---|
| Gravity | Fill level in the bottle | Bottle geometry varies |
| Volumetric | Chamber volume | Valve seal wears |
| Isobaric | Volume under counter-pressure | Pressure or temperature drifts |
| Piston | Displacement | Product carries solids |
| Load cell | Net weight | Product temperature moves |
A different bottle format means a different unit; see the Gravity Filling Machine for Still Water.
Valve count follows the target BPH and the fill time per valve. Longer fill time, thicker product or a taller bottle all reduce the rate per valve, so the same BPH needs more valves. Buying valves for a water duty and running juice on them is a common and expensive mismatch.
Where this becomes a line rather than a single machine, the Volumetric Filling Machine for Still Water is the starting point.
Foaming product needs a slower fill ramp and often a longer nozzle that reaches below the surface. The machine is the same frame with a different valve and a different cam or recipe. Sizing it on the water rate and hoping the foam settles is how lines end up at half output.
By considering the viscosity of your beverages and choosing appropriate filler types, you can enhance efficiency and product quality within your operations.
The same question is worked through from another angle in PET Bottle Design and Line Efficiency: Closures and Valve.
Yes, with change parts: star wheels, guide rails, grippers and a recipe. The parts are cheap compared with the changeover time, which is why most plants specify one dominant format.
From tens of minutes to over an hour, set by the circuit volume and the soil. It is a fixed cost per production day and should be planned as downtime, not squeezed into the shift.
Bottle capacity variation, product temperature, valve wear or foam. On glass, mould-to-mould capacity variation alone is enough to make level filling inconsistent, which is why glass lines often check-weigh.
Valve seals, piston seals, capping head inserts, guide rail blocks and one set of change parts for the second format. These are the items that stop a line for days when they fail.
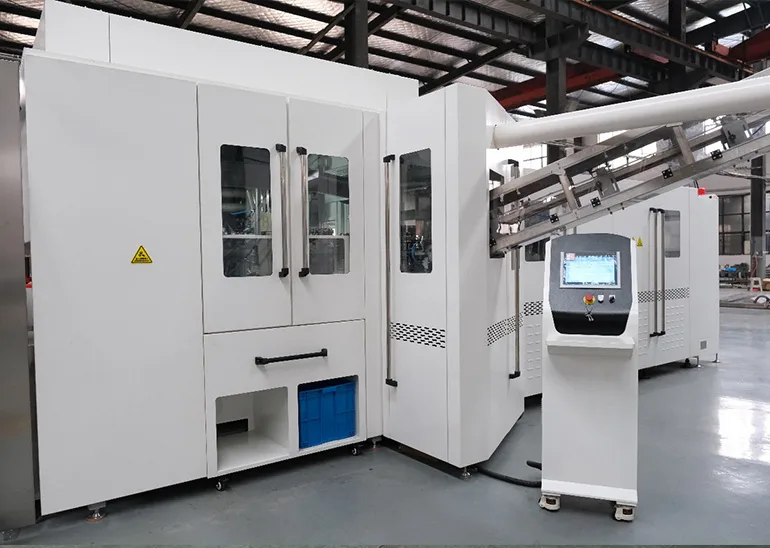
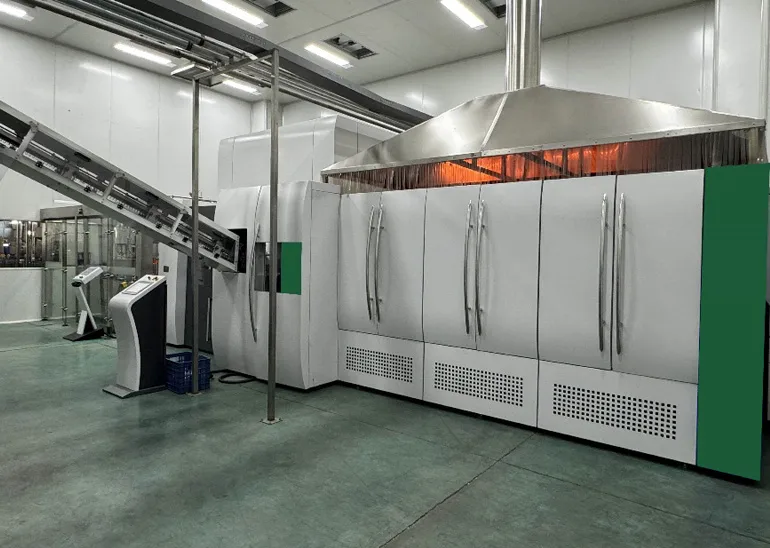
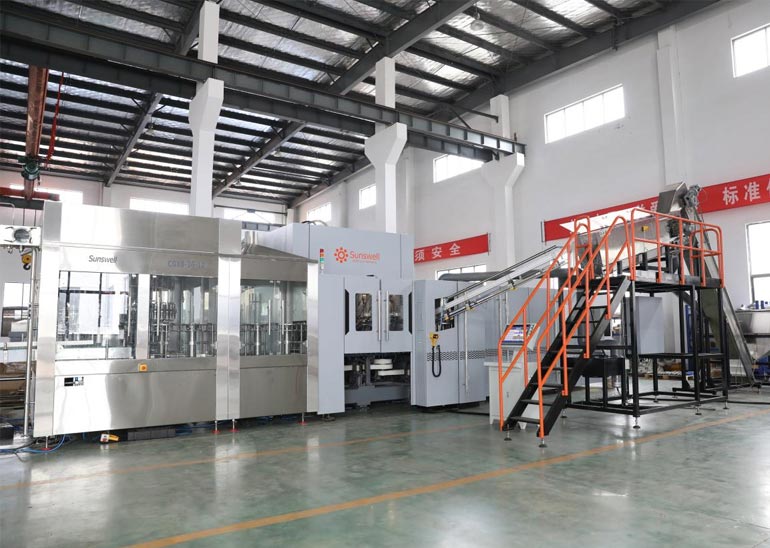
Country:Kazakhstan
Product: PET Bottled Sparkling Water, Canned Soft Drink, Canned Tea
Capacity: 25000CPH (250ml)
Solution:Three Lines,7000BPH(1.5L), 15000CPH(330ml),15000CPH(450ml)



 +86 13921964455
 [email protected]

A2 Dongjiu Industrial Park, 30 East Jintang Road, Tangshi, Zhangjiagang, Jiangsu 215600, China


