
| Supply scope | Filling, capping, labelling and packing equipment |
| Sizing basis | Demand in units per day, divided by productive hours and a production factor |
| Production factor | 0.65-0.85 depending on formats and changeovers |
| Key control | Fill accuracy, closure integrity, changeover time |
| Key decision | One flexible line or two dedicated lines |
| Acceptance | Output, accuracy, closure and changeover, measured |
Changeover, CIP, label roll changes and downstream stops. A line rated at 12,000 BPH and run with four formats and two changeovers per shift delivers closer to 8,000. The production factor is not a discount on the machine; it is what the plant actually gets.
Automated systems can adjust filling speeds, nozzle positions, and fill levels based on real-time temperature data, ensuring consistent performance throughout the production process.
It proves the machine meets the written specification on the agreed product, at the agreed format, in the builder workshop. It does not prove the line will run in your building. Both tests are needed, and the second one is where most disputes start.
| Decision | What it fixes | What it does not fix |
|---|---|---|
| Filling principle | Product and accuracy | Downstream capacity |
| Valve count | Rated BPH | Changeover and CIP time |
| Automation level | Labour per shift | Product quality |
| Line layout | Floor space and flow | Throughput of the slowest station |
A different bottle format means a different unit; see the Gravity Filling Machine for Still Water.
One full set of valve seals, one set of capping inserts, guide rail blocks and the change parts for the second format. These are the items with long lead times that stop a line for days. Buying them with the machine is cheaper than buying them in a hurry.
To maintain filling accuracy, it is imperative for bottling plants to make necessary adjustments based on the temperature of the product being processed.
The Volumetric Filling Machine for Still Water is the reference unit for this configuration.
By the cost of the labour it replaces and the consistency it adds, not by the technology. A robot palletizer pays on three shifts with a stable pattern; it does not pay on one shift with five patterns. The same logic applies to inspection and packing.
The same question is worked through from another angle in How to Improve Overall Equipment Effectiveness (OEE) in Bottling.
A well-maintained stainless line runs for well over a decade, with wear parts replaced on condition. The variables are water quality, cleaning regime and whether spare parts are kept in stock.
Capacity is usually added by a second line or by a downstream upgrade, not by speeding up the filler. The filler, the capper and the packer are matched, so raising one alone moves the bottleneck.
Valve count, automation level, material of construction, whether blowing is included, and the packing format. Price follows the specification, so two quotes are only comparable when the specifications match.
Between 0.65 and 0.85. A single-format line on one shift sits near 0.85; a line with four formats and two changeovers per shift sits near 0.65.
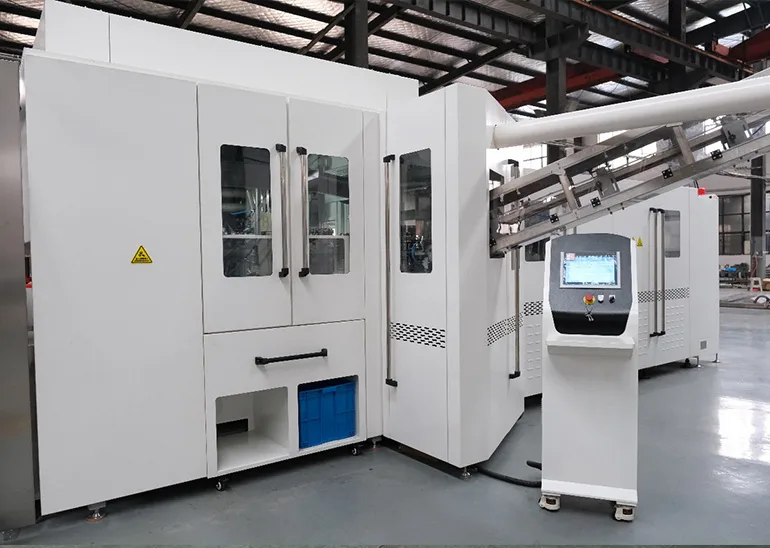
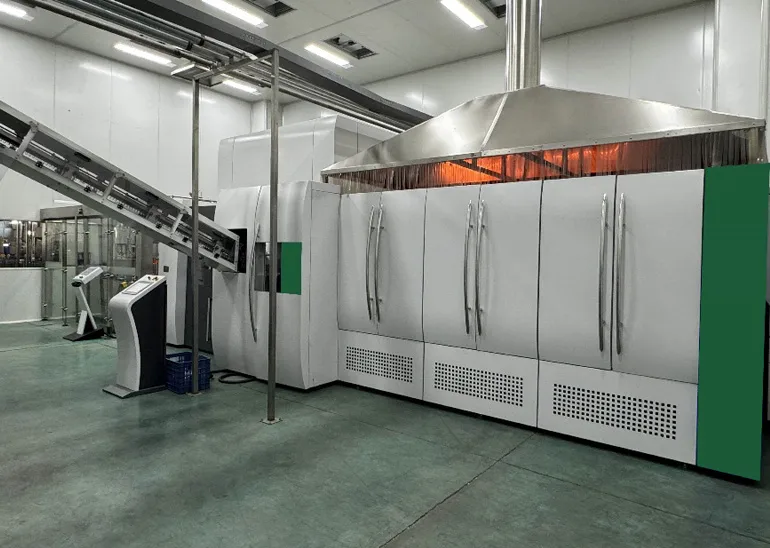
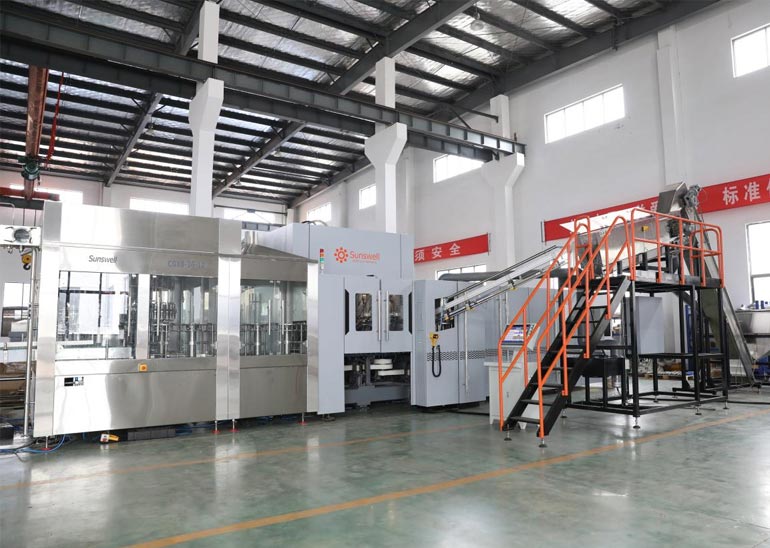
Country:Kazakhstan
Product: PET Bottled Sparkling Water, Canned Soft Drink, Canned Tea
Capacity: 25000CPH (250ml)
Solution:Three Lines,7000BPH(1.5L), 15000CPH(330ml),15000CPH(450ml)



 +86 13921964455
 [email protected]

A2 Dongjiu Industrial Park, 30 East Jintang Road, Tangshi, Zhangjiagang, Jiangsu 215600, China


