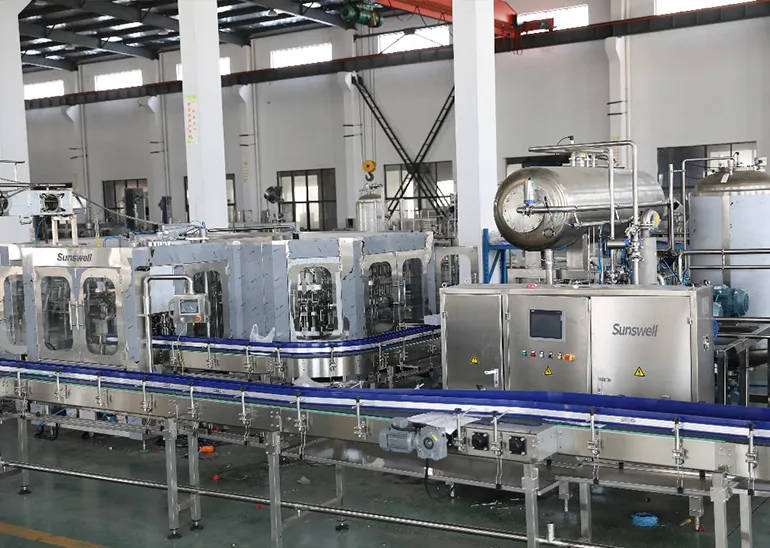
| Scope | Filling, capping, labelling and packing equipment |
| Sizing basis | Demand in units per day, divided by productive hours and a production factor |
| Production factor | 0.65-0.85 depending on formats and changeovers |
| Key control | Fill accuracy, closure integrity, changeover time |
| Key decision | One flexible line or two dedicated lines |
| Acceptance | Output, accuracy, closure and changeover, measured |
Settle the product and the package before the machine. Product viscosity, acidity, carbonation and particle size decide the filling principle; the bottle neck finish decides the capping head and the change parts. A machine chosen before those two are fixed is chosen twice.
Changeover, CIP, label roll changes and downstream stops. A line rated at 12,000 BPH and run with four formats and two changeovers per shift delivers closer to 8,000. The production factor is not a discount on the machine; it is what the plant actually gets.
When choosing a compressor for your bottling plant, consider factors such as required air pressure, flow rate, duty cycle, and energy efficiency.
| Decision | What it fixes | What it does not fix |
|---|---|---|
| Filling principle | Product and accuracy | Downstream capacity |
| Valve count | Rated BPH | Changeover and CIP time |
| Automation level | Labour per shift | Product quality |
| Line layout | Floor space and flow | Throughput of the slowest station |
The unit behind this configuration is the Gravity Filling Machine for Still Water.
At 1:100, with conveyor radii, maintenance access and the largest format drawn in. Most layout problems appear as a service door that cannot open or a pallet that cannot turn. Fixing them on paper costs nothing; fixing them on site costs weeks.
Sizing for this duty runs through the Volumetric Filling Machine for Still Water, where the valve count is set out.
One full set of valve seals, one set of capping inserts, guide rail blocks and the change parts for the second format. These are the items with long lead times that stop a line for days. Buying them with the machine is cheaper than buying them in a hurry.
The same question is worked through from another angle in How to Scope a Turnkey Beverage Bottling Plant in.
Bottles per day divided by productive hours, then divided by a production factor of 0.65-0.85. The factor covers changeover, cleaning and downstream stops. Sizing at 1.0 is the most common planning error.
A monoblock combines rinse, fill and cap on one frame. A full line adds treatment, blowing, labelling, packing and palletizing around it. The monoblock is one station in a longer chain.
Valve count, automation level, material of construction, whether blowing is included, and the packing format. Price follows the specification, so two quotes are only comparable when the specifications match.
Between 0.65 and 0.85. A single-format line on one shift sits near 0.85; a line with four formats and two changeovers per shift sits near 0.65.
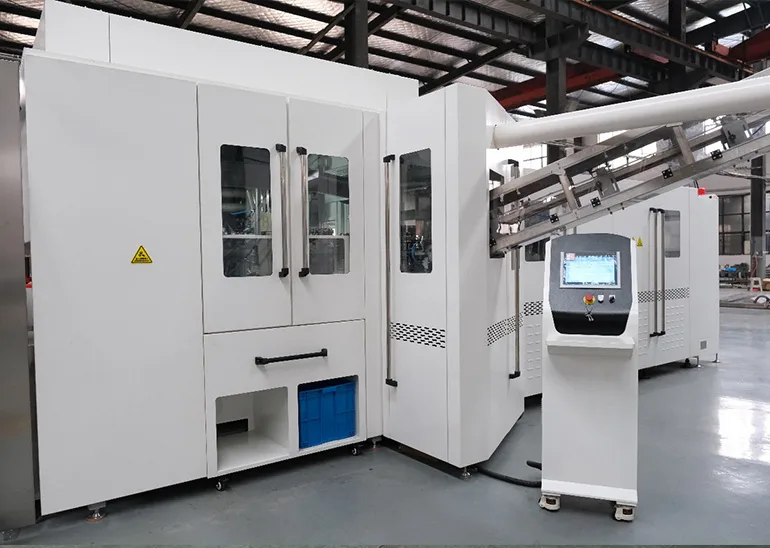
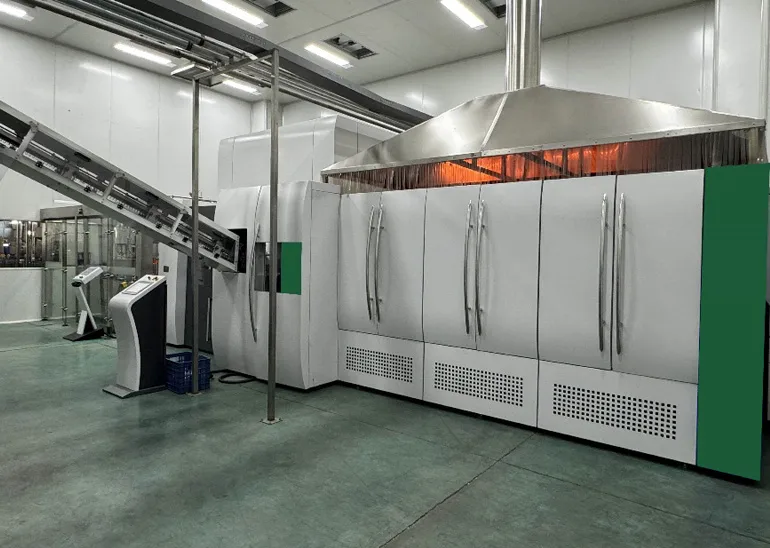
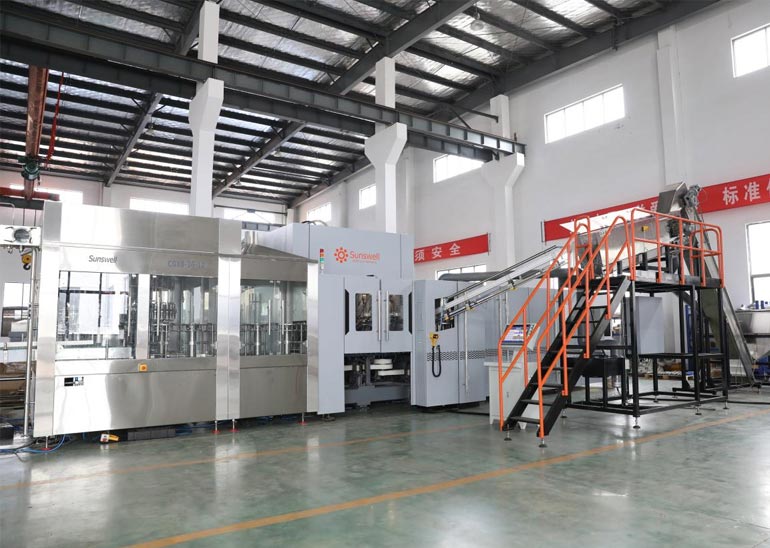
Country:Kazakhstan
Product: PET Bottled Sparkling Water, Canned Soft Drink, Canned Tea
Capacity: 25000CPH (250ml)
Solution:Three Lines,7000BPH(1.5L), 15000CPH(330ml),15000CPH(450ml)



 +86 13921964455
 [email protected]

A2 Dongjiu Industrial Park, 30 East Jintang Road, Tangshi, Zhangjiagang, Jiangsu 215600, China