
| Filling method | Isobaric, CO2 counter-pressure |
| Rated output | 12,000-36,000 BPH at 0.2-2 L |
| Containers | PET bottle, glass bottle, aluminum can |
| CO2 handling | Pre-pressurisation and return pipe, no venting |
| Valves | Mechanical, semi-electric or volumetric |
| Line scope | Water treatment, syrup mixing, carbonation, filler, pack |
Start from the symptom and work back to the mechanism, not from the part list. Most filling faults show up in three places: fill weight or level, closure integrity, and product condition. Which of the three moved first tells you whether the cause is mechanical, thermal or product-side.
The CO2 pressure applied during bottling directly affects the level of carbonation in CSDs and consequently, foam formation.
A carbonated drink is a saturated solution held in equilibrium by pressure and temperature. If the filler exposes it to atmosphere, CO2 leaves the liquid as foam and the fill level collapses. Isobaric filling pressurises the bottle to the bowl pressure first, fills under counter-pressure, then releases in a controlled ramp.
By optimizing valve timing, adjusting nozzles, and managing CO2 pressure effectively, you can significantly reduce foam levels and enhance the overall bottling process.
| Valve type | Setting | Best for |
|---|---|---|
| Mechanical | Fixed cam profile | Single product, long runs |
| Semi-electric | Signal-timed open and close | Recipe changes within one product family |
| Volumetric | Chamber dose | Pressure or temperature drift during the shift |
| Isobaric + volumetric | Chamber dose under counter-pressure | High CO2 with tight fill accuracy |
Site requirements, air and water consumption sit with the CSD & Sparkling Water by Mechanical Filler.
Foam is usually a temperature or pressure problem, not a valve problem. Warm product, a fast pressure release at the end of fill, a worn seal that lets gas bypass, or a dirty return pipe all show up as foam at the same place. Check the product temperature and the pressure ramp before touching the valves.
A different bottle format means a different unit; see the Isobaric Filling Machine for CSD and Sparkling Water.
Syrup is proportioned and blended with treated water, then carbonated under pressure and temperature control. The ratio accuracy and the carbonation stability decide the product, and both are upstream of the filler. A filler cannot correct a drifting blend.
The same question is worked through from another angle in Carbon Mixer at 15 C: How CO2 Retention Is.
Usually product temperature rising in the bowl or a worn valve seal. Both change the pressure balance, so the fill cuts off earlier. Log bowl temperature and fill weight together for one shift before changing any valve.
It is used where the package needs internal pressure support or low oxygen, for example in cans and in some PET formats. It is an option, not a default, and it adds a consumable cost per 1,000 units.
The higher the volumes, the sharper the mouthfeel and the more pressure the package must hold. Higher carbonation also needs a colder fill and a tighter pressure ramp, so it reduces practical line speed.
Yes, with a different infeed, spacing and capping set. Glass needs mechanical spacing rather than an air conveyor, and the filler runs at 4,000-20,000 BPH on glass against 12,000-36,000 BPH on PET.
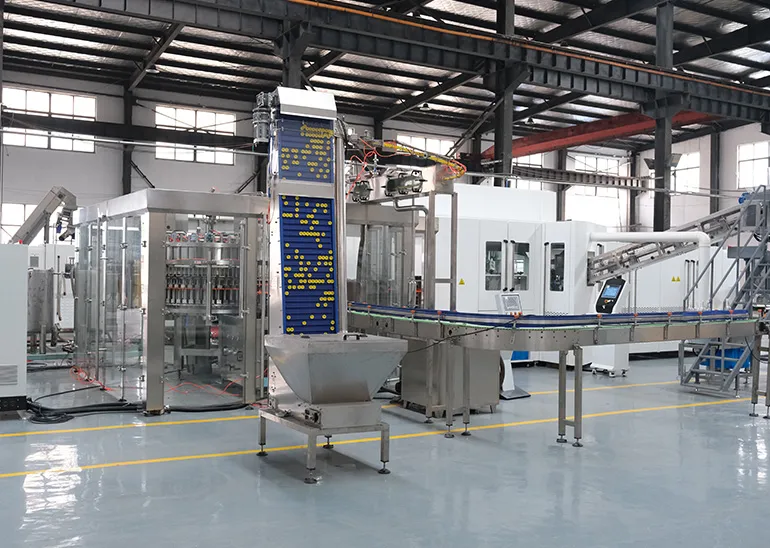
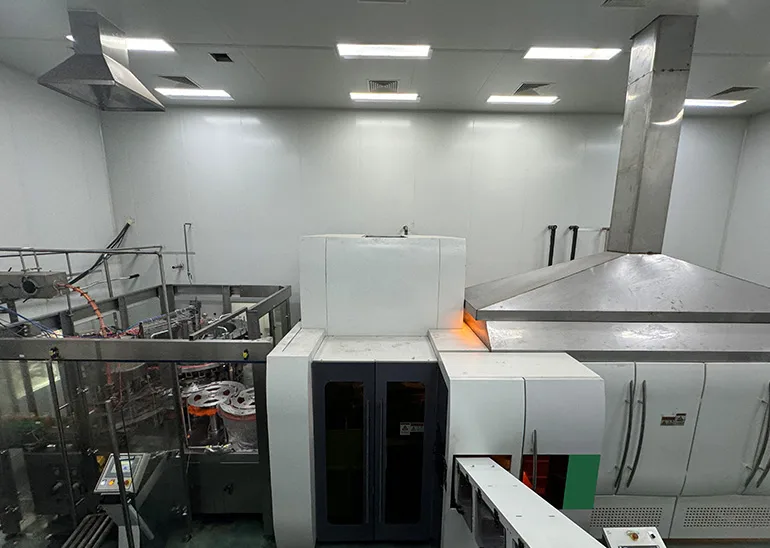
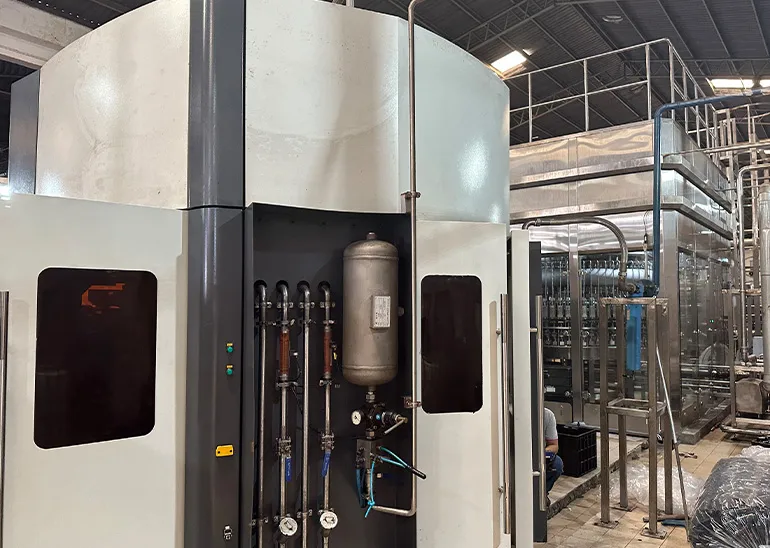
Country: Kazakhstan
Product: PET Bottled Carbonated Soft Drinks
Capacity: 12000BPH (1L)
Solution:Carbonated Drinks Production Line
Country: Syria
Product: Aluminum Canned Carbonated Soft Drinks
Capacity: 24000CPH (250ml)
Solution:Carbonated Drinks Production Line



 +86 13921964455
 [email protected]

A2 Dongjiu Industrial Park, 30 East Jintang Road, Tangshi, Zhangjiagang, Jiangsu 215600, China


