
| Filling system | Isobaric, CO2 counter-pressure |
| Rated output | 12,000-36,000 BPH at 0.2-2 L |
| Containers | PET bottle, glass bottle, aluminum can |
| CO2 handling | Pre-pressurisation and return pipe, no venting |
| Valves | Mechanical, semi-electric or volumetric |
| Line scope | Water treatment, syrup mixing, carbonation, filler, pack |
Size the filler on peak shift demand with a production factor of 0.65-0.85, then size the CO2 supply on average consumption, not peak. A CO2 plant built for the filler nameplate runs partly loaded for most of the year and loses more gas to vaporisation than the line saves in speed.
By prioritizing CO2 retention, foam control, and production efficiency, bottled water plants can enhance the quality, consistency, and output of their carbonated beverage lines.
Syrup is proportioned and blended with treated water, then carbonated under pressure and temperature control. The ratio accuracy and the carbonation stability decide the product, and both are upstream of the filler. A filler cannot correct a drifting blend.
Preserving the optimal levels of CO2 in carbonated beverages is a non-negotiable factor in maintaining the refreshing fizz and taste that consumers crave.
| Valve type | Setting | Best for |
|---|---|---|
| Mechanical | Fixed cam profile | Single product, long runs |
| Semi-electric | Signal-timed open and close | Recipe changes within one product family |
| Volumetric | Chamber dose | Pressure or temperature drift during the shift |
| Isobaric + volumetric | Chamber dose under counter-pressure | High CO2 with tight fill accuracy |
Sizing for this duty runs through the CSD & Sparkling Water by Mechanical Filler, where the valve count is set out.
A can is filled and seamed, a PET bottle is filled and capped. Cans run faster per unit and are counted in CPH; PET allows larger formats and a lighter package. The filler principle is the same isobaric one, the closing equipment and the line rate are not.
Rated output, change parts and services are listed on the Isobaric Filling Machine for CSD and Sparkling Water page.
Overfoaming is gas leaving the product too fast at the end of fill. The pressure release has to be ramped, not dumped, and the fill height has to leave the right headspace. A snift valve that opens too early turns a good fill into a wet bottle.
By focusing on CO2 retention, foam control, and production efficiency tips, we aim to equip you with invaluable insights to enhance your production processes.
The same question is worked through from another angle in Bottled Water vs CSD vs Juice: Which Segment Drives.
Usually product temperature rising in the bowl or a worn valve seal. Both change the pressure balance, so the fill cuts off earlier. Log bowl temperature and fill weight together for one shift before changing any valve.
400 cans per minute. CPH and BPH are different units and cannot be compared directly, because can and bottle formats carry different volumes and different downstream equipment.
It is used where the package needs internal pressure support or low oxygen, for example in cans and in some PET formats. It is an option, not a default, and it adds a consumable cost per 1,000 units.
Warm product and an empty bowl. The first bottles see the largest pressure step. A short recirculation before production and a controlled bowl cool-down remove most of it.
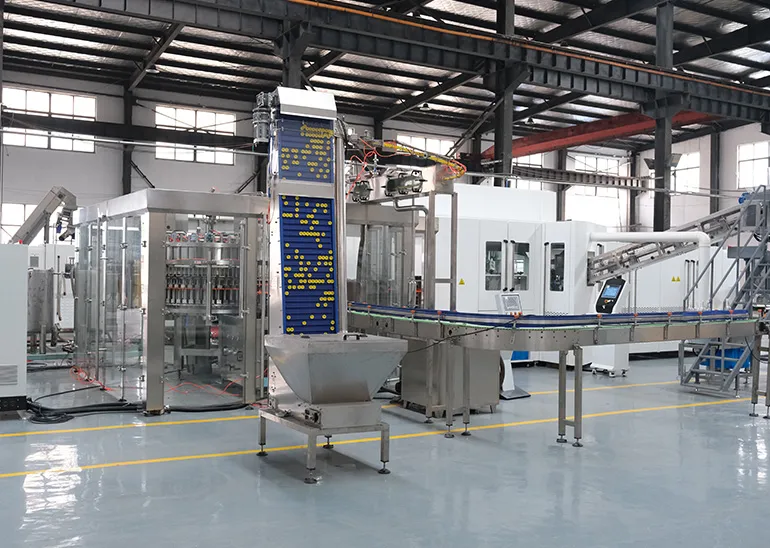
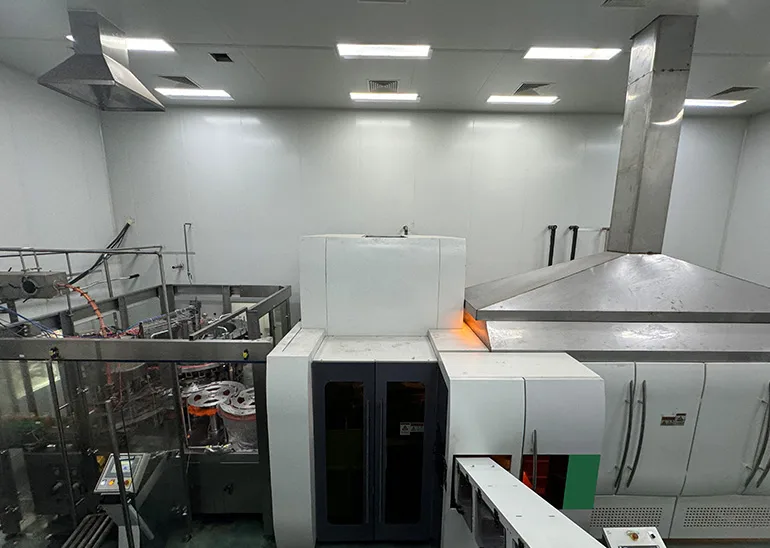
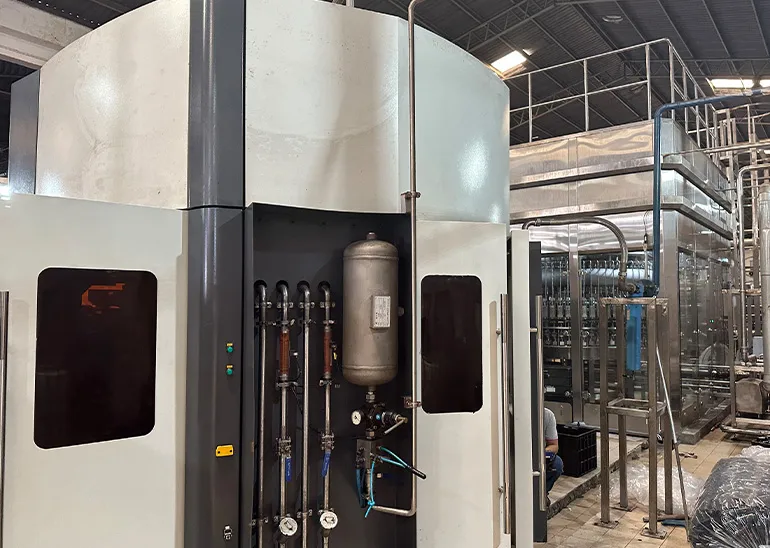
Country: Kazakhstan
Product: PET Bottled Carbonated Soft Drinks
Capacity: 12000BPH (1L)
Solution:Carbonated Drinks Production Line
Country: Syria
Product: Aluminum Canned Carbonated Soft Drinks
Capacity: 24000CPH (250ml)
Solution:Carbonated Drinks Production Line



 +86 13921964455
 [email protected]

A2 Dongjiu Industrial Park, 30 East Jintang Road, Tangshi, Zhangjiagang, Jiangsu 215600, China


