
| Valve type | Isobaric, CO2 counter-pressure |
| Capacity | 12,000-36,000 BPH at 0.2-2 L |
| Containers | PET bottle, glass bottle, aluminum can |
| CO2 handling | Pre-pressurisation and return pipe, no venting |
| Valves | Mechanical, semi-electric or volumetric |
| Line scope | Water treatment, syrup mixing, carbonation, filler, pack |
Start from the symptom and work back to the mechanism, not from the part list. Most filling faults show up in three places: fill weight or level, closure integrity, and product condition. Which of the three moved first tells you whether the cause is mechanical, thermal or product-side.
Another critical aspect that directly affects foam levels in CSD filling lines is the control of CO2 pressure.
A carbonated drink is a saturated solution held in equilibrium by pressure and temperature. If the filler exposes it to atmosphere, CO2 leaves the liquid as foam and the fill level collapses. Isobaric filling pressurises the bottle to the bowl pressure first, fills under counter-pressure, then releases in a controlled ramp.
High CO2 pressure can lead to aggressive bubbling, resulting in increased foam production.
| Valve type | Setting | Best for |
|---|---|---|
| Mechanical | Fixed cam profile | Single product, long runs |
| Semi-electric | Signal-timed open and close | Recipe changes within one product family |
| Volumetric | Chamber dose | Pressure or temperature drift during the shift |
| Isobaric + volumetric | Chamber dose under counter-pressure | High CO2 with tight fill accuracy |
A different bottle format means a different unit; see the CSD & Sparkling Water by Mechanical Filler.
Mechanical valves open and close on a fixed cam profile and are the most forgiving on maintenance. Semi-electric valves use a signal to open and close, so the fill window can be set per recipe. Volumetric valves dose a chamber and hold accuracy when bottle pressure or product temperature drifts during the shift.
By focusing on valve timing optimization, CO2 pressure control, and machine setup and maintenance, you can effectively minimize foam generation and streamline the filling process.
Site requirements, air and water consumption sit with the Isobaric Filling Machine for CSD and Sparkling Water.
Foam is usually a temperature or pressure problem, not a valve problem. Warm product, a fast pressure release at the end of fill, a worn seal that lets gas bypass, or a dirty return pipe all show up as foam at the same place. Check the product temperature and the pressure ramp before touching the valves.
By maintaining optimal pressure control, you can effectively reduce foam generation and improve the overall quality of the filled product.
The same question is worked through from another angle in How Gravity Fillers Reduce Oxidation in Sparkling Drinks.
It holds what the mixer sets and the temperature allows. Most CSD runs between 2.5 and 4.0 volumes, with the target set per product. Retention, not the mixer set point, is what the acceptance test should measure in the filled bottle.
400 cans per minute. CPH and BPH are different units and cannot be compared directly, because can and bottle formats carry different volumes and different downstream equipment.
The higher the volumes, the sharper the mouthfeel and the more pressure the package must hold. Higher carbonation also needs a colder fill and a tighter pressure ramp, so it reduces practical line speed.
Yes, with a different infeed, spacing and capping set. Glass needs mechanical spacing rather than an air conveyor, and the filler runs at 4,000-20,000 BPH on glass against 12,000-36,000 BPH on PET.
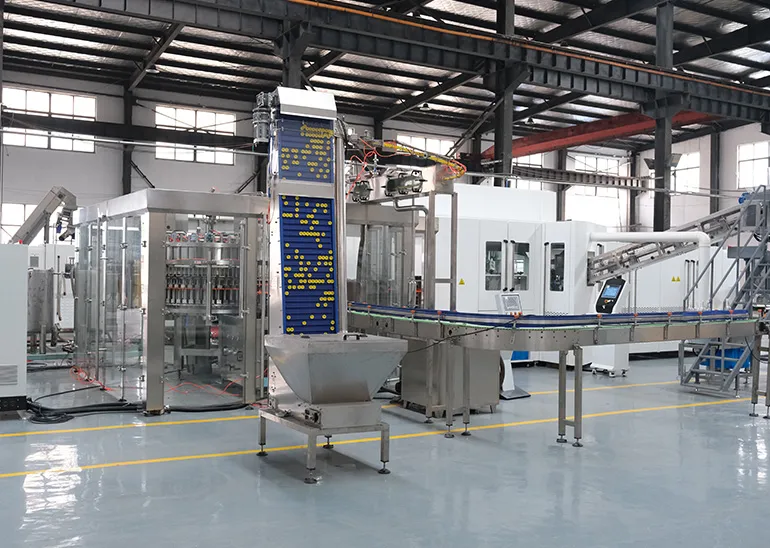
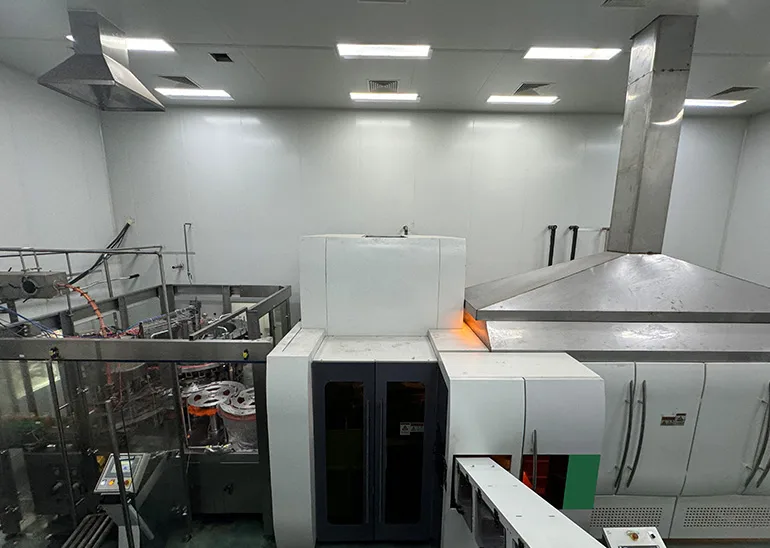
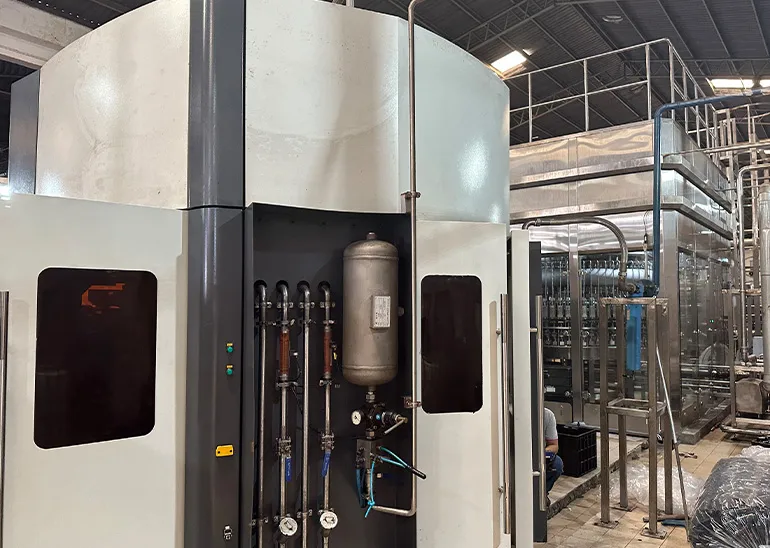
Country: Kazakhstan
Product: PET Bottled Carbonated Soft Drinks
Capacity: 12000BPH (1L)
Solution:Carbonated Drinks Production Line
Country: Syria
Product: Aluminum Canned Carbonated Soft Drinks
Capacity: 24000CPH (250ml)
Solution:Carbonated Drinks Production Line



 +86 13921964455
 [email protected]

A2 Dongjiu Industrial Park, 30 East Jintang Road, Tangshi, Zhangjiagang, Jiangsu 215600, China


