
| Filling principle | Isobaric for beer and CSD, volumetric for juice and tea |
| Output range | Up to 25,000 CPH |
| Can sizes | Standard 250, 330 and 500 ml |
| Seaming | Roller seamer integrated with the filler |
| Options | Hot fill for juice and tea, nitrogen dosing |
| Key control | Fill level, seam tightness, dissolved oxygen |
Maintenance effort should follow the wear map, not the machine layout. Seals, capping inserts, guide rail blocks and filters account for most unplanned stops; painting and polishing account for none. A short daily check on those four items beats a long monthly inspection.
A can line is counted in cans per hour because the container is the unit the seamer closes. CPH and BPH cannot be converted without the fill volume, and the downstream packer is sized in cases per hour. Comparing a 24,000 CPH can line with a 24,000 BPH bottle line compares two different plants.
| Product | Filling principle | Critical measurement |
|---|---|---|
| Beer | Isobaric, cold | Dissolved oxygen and seam tightness |
| CSD and soda | Isobaric, cold | CO2 retention and fill height |
| Juice and tea | Volumetric or hot fill | Fill temperature and seam integrity |
| Energy drinks | Isobaric or volumetric | Dissolved oxygen and closure |
Site requirements, air and water consumption sit with the Aluminum Can Filling Machine for Beer, Carbonated Soft Drink.
Dissolved oxygen enters at three points: deaeration of the product, the filler bowl atmosphere, and the gap between fill and seam. Nitrogen dosing and a steam or CO2 tunnel at the seamer reduce the last one. For beer and juice, the dissolved oxygen in the finished can is the number to test, not the setting on the doser.
The unit behind this configuration is the Aluminum Can Filling Machine for Hotfill Juice and Tea.
Compressed air for the seamer and the air conveyor, CO2 for purging, and the tear-down cans used for seam checks every shift. None of these appear in the machine price. A line running 24,000 CPH can consume a measurable share of its operating cost in air alone.
The same question is worked through from another angle in Exploring Alternative Packaging: Aluminum Can Water Filling Lines.
It is the oxygen left in the product after filling. It drives oxidation, off-flavour and haze. Beer and juice have tight limits, and the measurement belongs in the acceptance protocol, taken from the finished can.
It is common for beer, juice and some CSD, where headspace oxygen has to be pushed down. It is an option with a consumable cost, so it belongs in the utility and consumable schedule, not in the base price.
Usually conveyor pressure or a jam at a transfer, not the can quality. Air conveyor pressure, guide rail gaps and accumulation length are the three settings to check first.
Yes, at the same filler, because the fill volume per cycle is smaller. The seamer and the packer still have to carry the higher can rate, which is why the line rating is set on cans per hour, not litres.
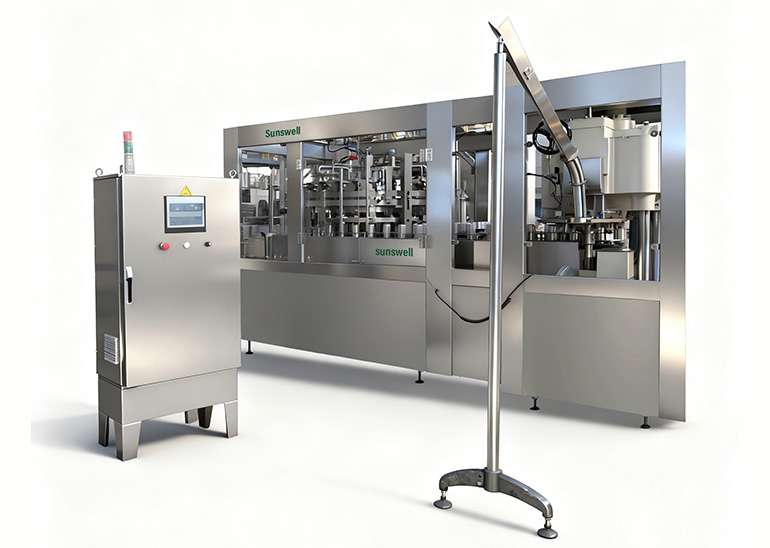
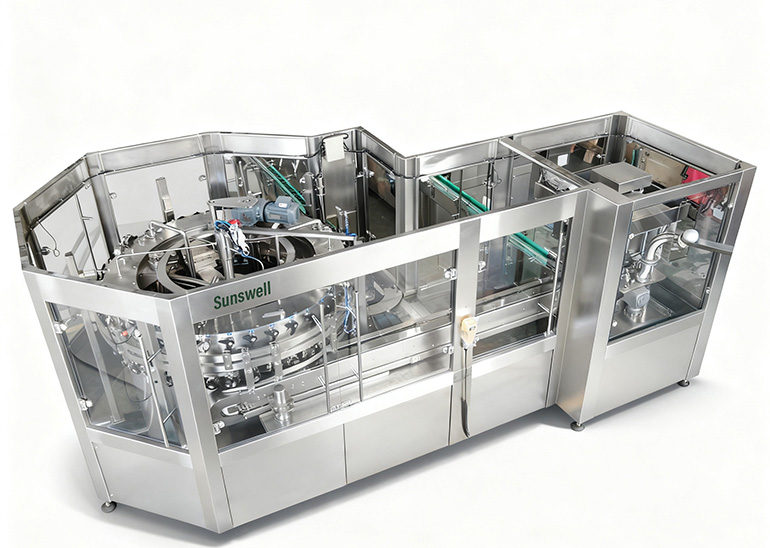
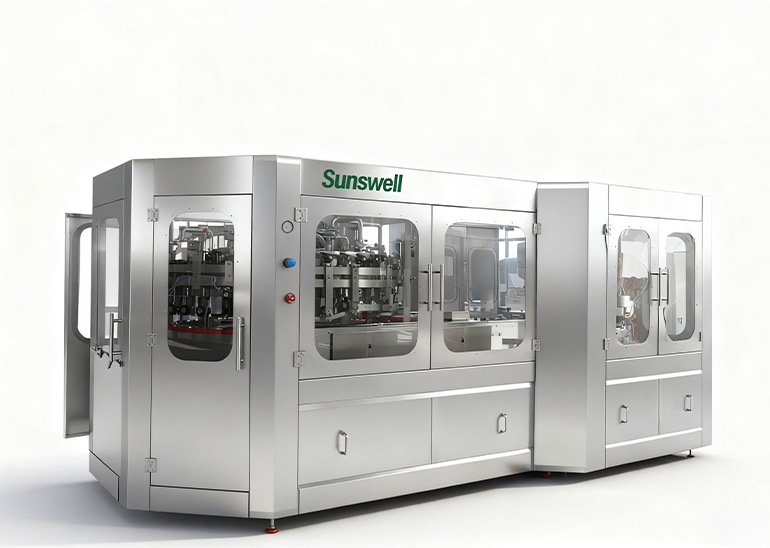
Country: Syria
Product: Aluminum Canned Carbonated Soft Drinks
Capacity: 24000CPH (250ml)
Solution:Carbonated Drinks Production Line
Country:Kazakhstan
Product: PET Bottled Sparkling Water, Canned Soft Drink, Canned Tea
Capacity: 25000CPH (250ml)
Solution:Three Lines,7000BPH(1.5L), 15000CPH(330ml),15000CPH(450ml)



 +86 13921964455
 [email protected]

A2 Dongjiu Industrial Park, 30 East Jintang Road, Tangshi, Zhangjiagang, Jiangsu 215600, China


