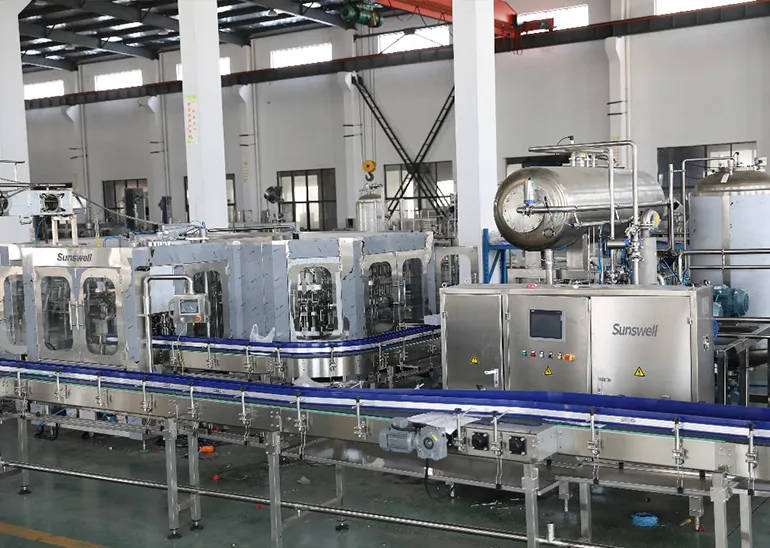
| Filling principle | Hot-fill, up to 85 C |
| Capacity range | 6,000-36,000 BPH at 0.2-2 L |
| Bottle | Heat-resistant PET geometry, or glass |
| Line | Hot-fill monobloc with tunnel pasteuriser |
| Products | Juice, tea, nectar, functional drinks |
| Key control | Fill temperature, hold time, cap seal |
Hot filling does two jobs at once: it pasteurises the product on the way to the filler, and the residual heat sanitises the bottle and cap. That is why a hot-fill line can run an acidic juice without a separate bottle steriliser. The price is a heat-resistant bottle and a longer cooling tunnel.
By adhering to precise temperature control, optimizing flow rates, and prioritizing microbial reduction, bottled water plants can uphold the highest standards of hygiene and consumer protection.
Tea usually needs finer filtration, deaeration to protect aroma, and a fill temperature that does not strip the volatile notes. Tea also clouds after cooling, so the clarification step is part of the product design, not a filling detail.
Maintaining an optimal flow rate ensures uniform heat distribution throughout the product, guaranteeing that all particles are exposed to the necessary temperature for the required duration.
| Route | Temperature | What it costs |
|---|---|---|
| Hot fill | Up to 85 C | Heat-resistant bottle and a cooling tunnel |
| Cold fill with preservative | Ambient | Formulation constraint, not a machine constraint |
| Cold fill with in-line pasteuriser | Product-side only | Separate pasteuriser and a closed filling zone |
| Hot fill in glass | Up to 85 C | Glass mass, slower line, higher transport cost |
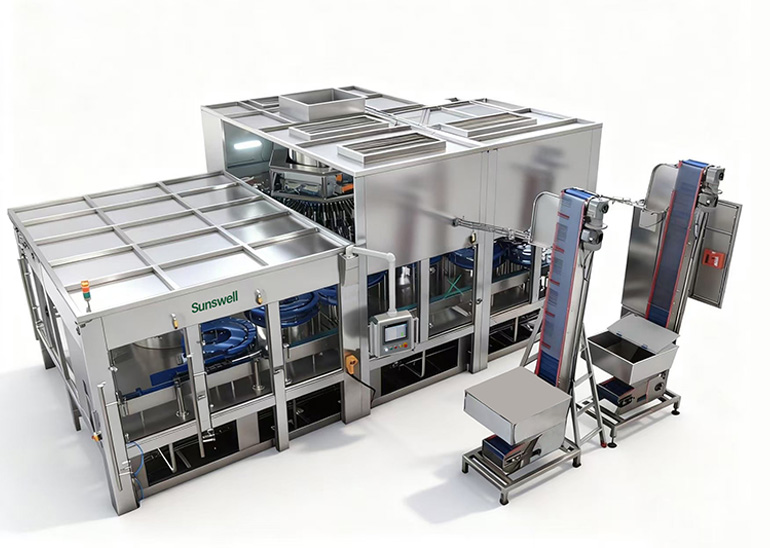
Where this becomes a line rather than a single machine, the Hotfill Type Filling Machine for Juice is the starting point.
The bottle leaves the filler at up to 85 C and has to come down in a controlled ramp. A plunge cools the outside first, the inside contracts later, and the panel pulls in. The tunnel zones are set per bottle geometry and checked with a probe in the product.
The optimal temperature range typically falls between 160°F to 180°F (71°C to 82°C), ensuring the destruction of harmful bacteria while maintaining the sensory attributes of the beverage.
The Juice By Volumetric Filler is the reference unit for this configuration.
Glass brings mass, breakage and a slower line. It also brings a closure decision: crown, lug or screw. A glass hot-fill line usually runs at a lower rate than the same filler on PET, and the difference is handling and inspection, not the valve.
The same question is worked through from another angle in Hotfill Juice in Glass: Cooling Tunnel and Tea-Side Differences.
Up to 85 C, set per product and per bottle. The exact set point and tolerance belong in the product specification, because acidity, pulp content and bottle wall thickness all move it.
No. Standard PET softens and deforms at fill temperature. The bottle needs a heat-resistant geometry, and the mould and preform are part of the project, not an afterthought.
Heat-sensitive pigments and vitamins degrade above the product temperature limit. The fill temperature and the hold time are the two variables; lowering either protects colour and shortens the microbial margin.
A controlled ramp rather than a cold plunge, so the bottle does not deform under vacuum. The tunnel zones are set per bottle geometry and validated with a temperature probe in the product.
Country:Kazakhstan
Product: PET Bottled Sparkling Water, Canned Soft Drink, Canned Tea
Capacity: 25000CPH (250ml)
Solution:Three Lines,7000BPH(1.5L), 15000CPH(330ml),15000CPH(450ml)



 +86 13921964455
 [email protected]

A2 Dongjiu Industrial Park, 30 East Jintang Road, Tangshi, Zhangjiagang, Jiangsu 215600, China