
| Supply scope | Printers, coders, cap feeders, nitrogen dosers, detectors |
| Function | Support the filler without changing its rating |
| Key control | Position, timing, consumable cost |
| Integration | Signals from the filler PLC or a standalone sensor |
| Key decision | Whether the device earns its cost per 1,000 units |
| Typical position | After the filler, before the packer |
Ink, solvent, laser power, nitrogen, caps and labels all carry a per-unit cost that does not appear in the machine price. A device with a low purchase price and a high consumable cost can be the most expensive item on the line over five years.
By carefully controlling the introduction of nitrogen during the filling process, bottling plants can regulate the pressure inside the bottle, preventing CO2 loss and maintaining the effervescence that consumers expect.
Either through a discrete signal from the filler PLC, which is simple and reliable, or through the line network, which allows recipes and reporting. Discrete signals are easier to commission; network integration is easier to audit. Choose based on who will maintain it.
| Device | What it controls | Consumable |
|---|---|---|
| Coder or printer | Date and batch code | Ink, solvent or laser power |
| Cap feeder | Cap supply to the capper | None, but a buffer is needed |
| Nitrogen doser | Headspace oxygen | Nitrogen per 1,000 units |
| Fill level detector | Reject decision | None, but a reject gate is needed |
Rated output, change parts and services are listed on the Accessory page.
Run the device at the line rating, not at a demonstration speed, and count rejects with the device on and off. Acceptance at half speed hides the timing problem that appears in the first production week.
By preventing oxidation, maintaining CO2 levels, and extending product shelf life, plant managers can elevate the quality and freshness of their bottled drinks to meet the evolving demands of consumers.
The specification sheet for the Conveying carries the figures quoted here.
Through an encoder on the conveyor, so the print position follows the actual speed rather than a set value. Without the encoder, the code stretches when the line accelerates and lands off-centre.
The same question is worked through from another angle in Tray Packer: When a Tray Beats a Full Shrink.
A consistent cap, a correct chute angle and a hopper that is never empty. Most cap jams are the chute and the level, not the sorter. A low-level sensor that stops the line before the hopper empties prevents most of them.
No. It does not change the filler rating. It reduces headspace oxygen, which protects shelf life. Its value is measured in shelf life and rejects, not in BPH.
Because the hopper is sized for a shift rather than for the line rate, or because the elevator runs slower than the capper consumes. Size the hopper on caps per minute at the filler rating, with margin.
Caps arrive out of orientation, the elevator runs faster than the chute can release, or the chute angle is wrong for the cap. Most jams are a chute and speed setting, not a cap defect.
Yes. Detection without a reject gate only records the defect. The gate needs a shift register so it rejects the bottle that was measured, not the one behind it.
Between the filler and the closure, close enough that the gas stays in the headspace. Moving it further downstream wastes gas and gives an unstable result.
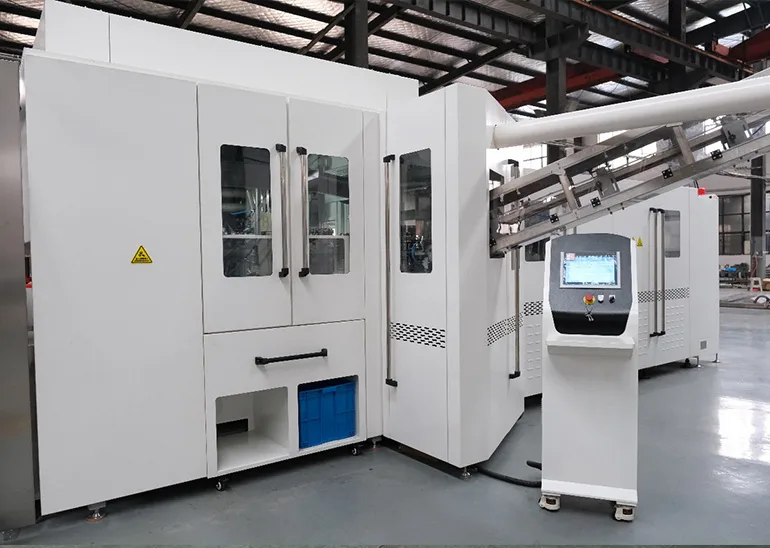
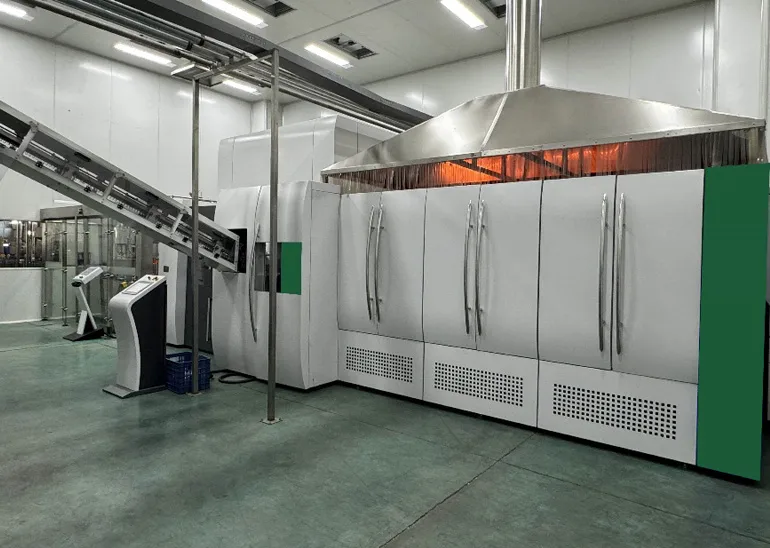
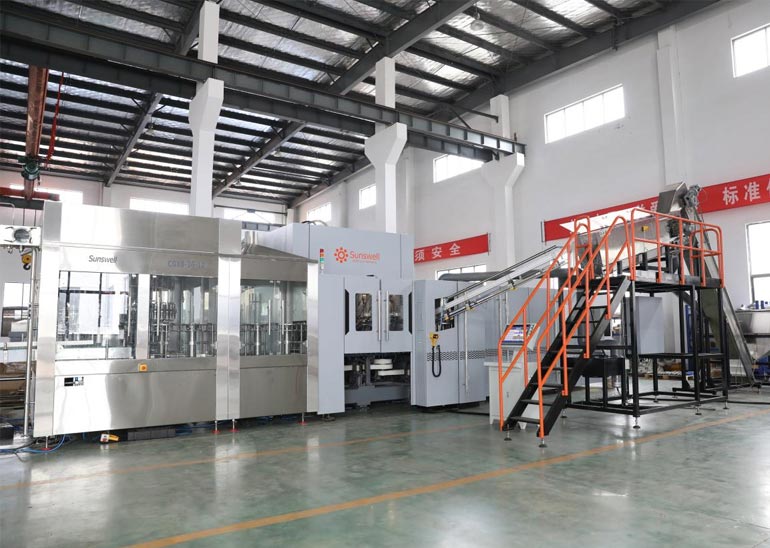
Country:Kazakhstan
Product: PET Bottled Sparkling Water, Canned Soft Drink, Canned Tea
Capacity: 25000CPH (250ml)
Solution:Three Lines,7000BPH(1.5L), 15000CPH(330ml),15000CPH(450ml)



 +86 13921964455
 [email protected]

A2 Dongjiu Industrial Park, 30 East Jintang Road, Tangshi, Zhangjiagang, Jiangsu 215600, China


