
| Combines | Blow moulding, filling and capping in one block |
| Rated output | 2,000-48,000 BPH |
| Bottle sizes | 0.2-16 L PET |
| Products | Still water, CSD, juice, tea, edible oil |
| Valves | Load cell, volumetric, mechanical or semi-electric |
| Operation | One operator for the complete block |
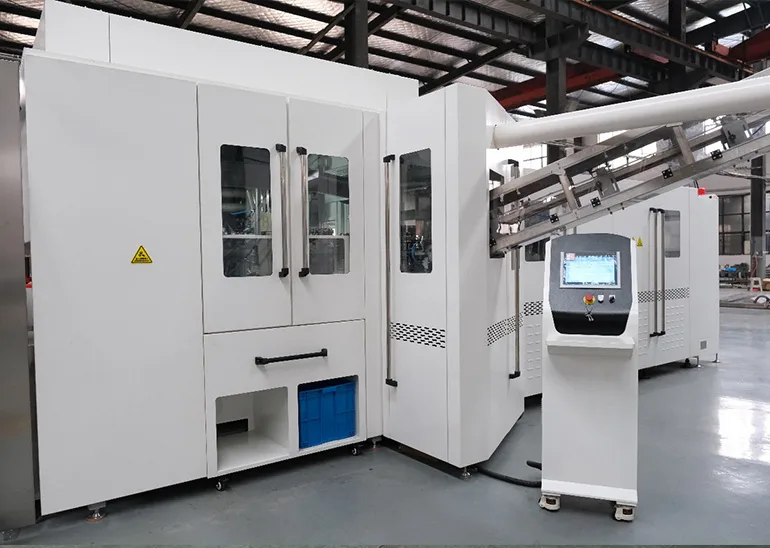
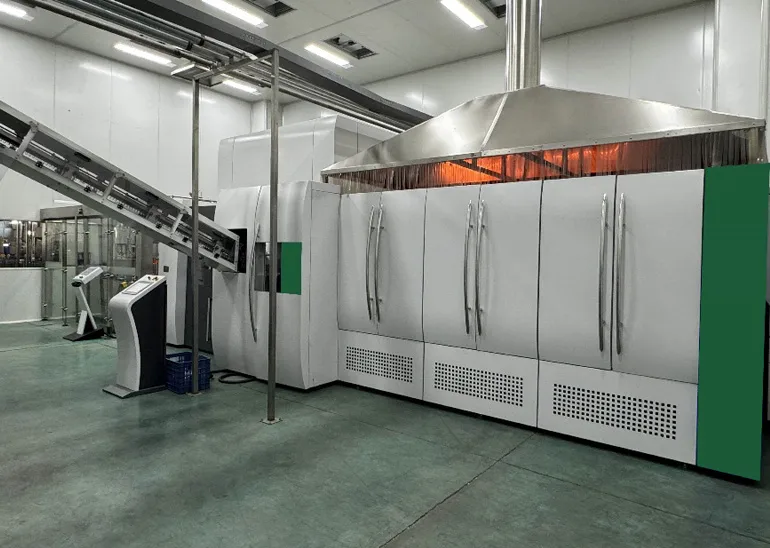
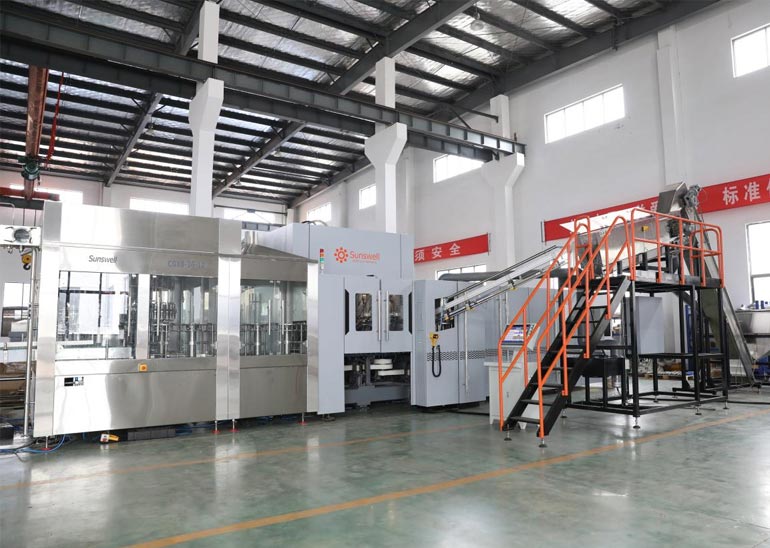
A combiblock joins blow moulding, filling and capping into one frame with one drive and one control system. The preform goes in at one end and the capped bottle comes out at the other, with no intermediate buffer and no bottle storage between blowing and filling.
A single footprint, a level floor, high-pressure air for blowing, chilled water for the mould, and power for the whole block on one feed. Because the machines are mechanically linked, the foundation and the levelling matter more than on three separate machines, and the installation sequence is fixed.
By utilizing load cells, managers can move away from volumetric measurements, which may be impacted by factors such as temperature variations and air pressure changes.
| Configuration | What is inside | Typical use |
|---|---|---|
| 3-in-1 monoblock | Rinse, fill, cap | Still water in bought bottles |
| Combiblock | Blow, fill, cap | PET lines with in-house blowing |
| Combiblock + labeller | Blow, fill, cap, label | Single-footprint PET line |
| Combiblock + packer | Blow to case | High-volume single-format plant |
Valve count, utility schedule and footprint sit on the Still Water 5L Volumetric page.
With a positive-pressure enclosure over the blow-fill-cap path, filtered air, and a defined cleaning cycle for the filler and the capper. The bottle is formed, filled and closed inside the same zone, which is the reason the format exists.
Valve count, utility schedule and footprint sit on the Blow-fill-cap Combibloc for Still Water page.
At the discharge of the block, in good capped bottles per hour, including the stops caused by blowing. Measuring at the filler alone flatters the number, because the filler waits for the blower more often than the other way round.
The same question is worked through from another angle in How Load Cells Improve Combibloc Filling Accuracy.
A monoblock combines rinsing, filling and capping. A combiblock adds blow moulding, so the preform goes in and the capped bottle comes out. The two terms are often confused, and the difference is whether a blow moulder is inside the block.
It is designed for one operator on the complete block, which is fewer people than three separate machines need. The saving is real only if the plant also removes the buffer and the bottle handling between stations.
The filler stops within seconds because there is no accumulation. That is why the uptime target for a combiblock is set for the block, not for each machine, and why preventive maintenance on the blower is not optional.
It removes the empty-bottle buffer and the conveyor between the blower and the filler, which is the largest space item on a conventional PET line. The exact saving depends on the buffer length in the original layout.
Country: Kazakhstan
Product: PET Bottled Carbonated Soft Drinks
Capacity: 12000BPH (1L)
Solution:Carbonated Drinks Production Line
Country: Maldives
Product: PET Bottled Mineralized Water
Capacity: 24,000BPH (500ml); 2 Lines
Solution:Water Production Line



 +86 13921964455
 [email protected]

A2 Dongjiu Industrial Park, 30 East Jintang Road, Tangshi, Zhangjiagang, Jiangsu 215600, China


