
| Filling principle | Isobaric for beer and CSD, volumetric for juice and tea |
| Capacity range | Up to 25,000 CPH |
| Can sizes | Standard 250, 330 and 500 ml |
| Seaming | Roller seamer integrated with the filler |
| Options | Hot fill for juice and tea, nitrogen dosing |
| Key control | Fill level, seam tightness, dissolved oxygen |
A can line is counted in cans per hour because the container is the unit the seamer closes. CPH and BPH cannot be converted without the fill volume, and the downstream packer is sized in cases per hour. Comparing a 24,000 CPH can line with a 24,000 BPH bottle line compares two different plants.
A can is sealed by two rolling operations that fold the can flange and the end together. Seam thickness, seam height and overlap are checked by tear-down at a fixed interval, not by eye. A seam that looks right and measures wrong leaks three weeks later, in the customer warehouse rather than on your line.
This high temperature poses a risk to the integrity of the aluminum cans, leading to potential deformation or leakage if not properly managed during the filling process.
| Product | Filling principle | Critical measurement |
|---|---|---|
| Beer | Isobaric, cold | Dissolved oxygen and seam tightness |
| CSD and soda | Isobaric, cold | CO2 retention and fill height |
| Juice and tea | Volumetric or hot fill | Fill temperature and seam integrity |
| Energy drinks | Isobaric or volumetric | Dissolved oxygen and closure |
Site requirements, air and water consumption sit with the Aluminum Can Filling Machine for Beer, Carbonated Soft Drink.
Beer and CSD run isobaric, cold, under counter-pressure. Juice and tea often run hot fill or a volumetric fill with a downstream pasteuriser. The can is the same format; the filler, the valve set and the temperature control are not, so one can line rarely covers both without a second specification.
Hotfill beverages, such as tea drinks and juices, are filled at high temperatures to ensure product safety and preservation.
The Aluminum Can Filling Machine for Hotfill Juice and Tea is the matching unit when this becomes a line project.
A heated product path, a fill temperature control loop and a cooling tunnel after seaming. The can itself tolerates the heat; the lining and the product do not always. The temperature window belongs to the product specification.
These machines are designed to withstand the high temperatures involved in the hotfill process and ensure the integrity of the cans throughout the filling operation.
The same question is worked through from another angle in How to Optimize Label Placement on Aluminum Cans.
300 cans per minute. Divide CPH by 60. The seamer, the filler and the packer all have to carry that number, so the line rating is the lowest of the three.
It is common for beer, juice and some CSD, where headspace oxygen has to be pushed down. It is an option with a consumable cost, so it belongs in the utility and consumable schedule, not in the base price.
Usually conveyor pressure or a jam at a transfer, not the can quality. Air conveyor pressure, guide rail gaps and accumulation length are the three settings to check first.
Usually seamer roll pressure, chuck wear or a can flange outside tolerance. The tear-down measures the result; the cause is found by checking the rolls and the can supplier specification together.
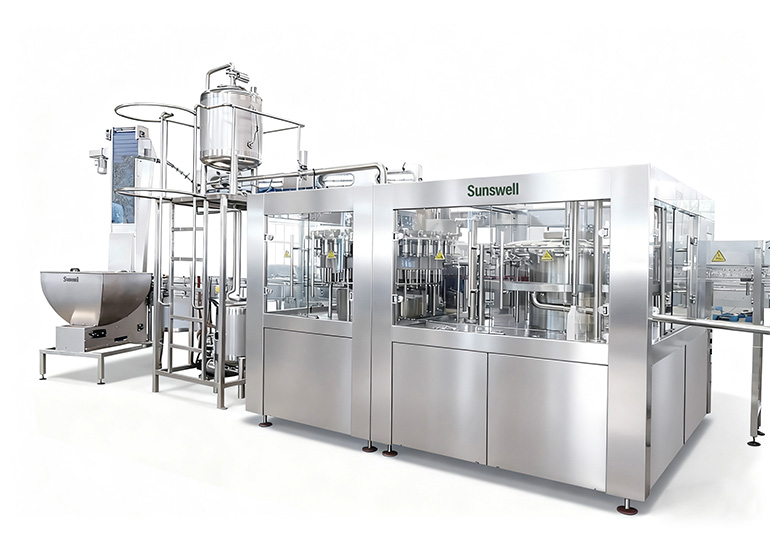
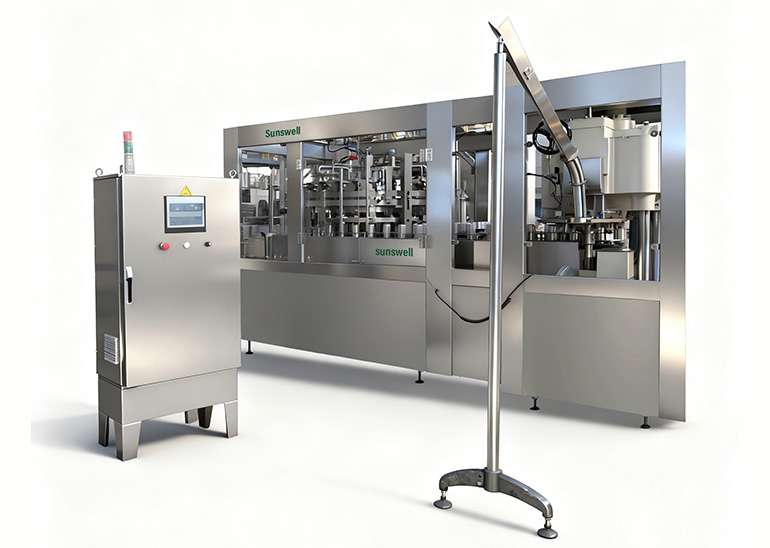
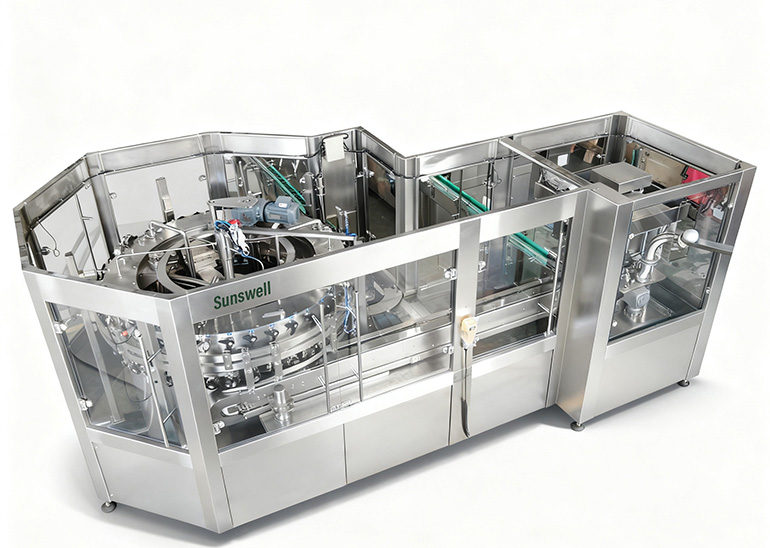
Country: Syria
Product: Aluminum Canned Carbonated Soft Drinks
Capacity: 24000CPH (250ml)
Solution:Carbonated Drinks Production Line
Country:Kazakhstan
Product: PET Bottled Sparkling Water, Canned Soft Drink, Canned Tea
Capacity: 25000CPH (250ml)
Solution:Three Lines,7000BPH(1.5L), 15000CPH(330ml),15000CPH(450ml)



 +86 13921964455
 [email protected]

A2 Dongjiu Industrial Park, 30 East Jintang Road, Tangshi, Zhangjiagang, Jiangsu 215600, China


