
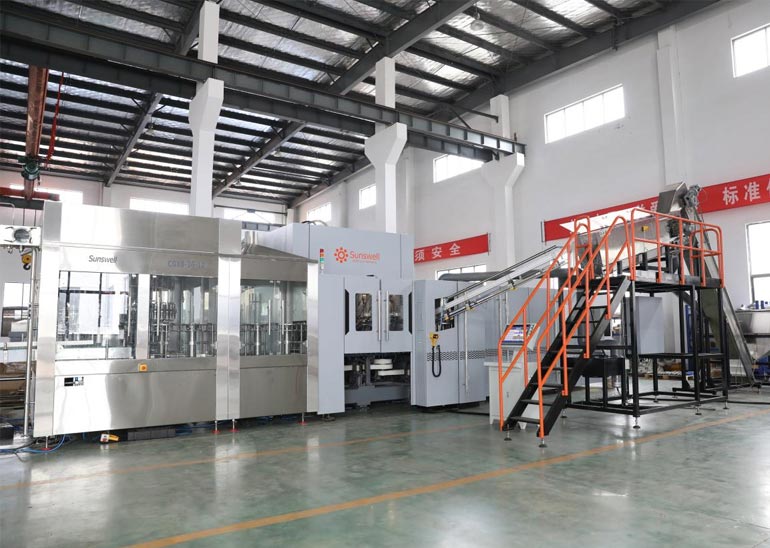
| Combines | Blow moulding, filling and capping in one block |
| Output range | 2,000-48,000 BPH |
| Container range | 0.2-16 L PET |
| Products | Still water, CSD, juice, tea, edible oil |
| Valves | Load cell, volumetric, mechanical or semi-electric |
| Operation | One operator for the complete block |
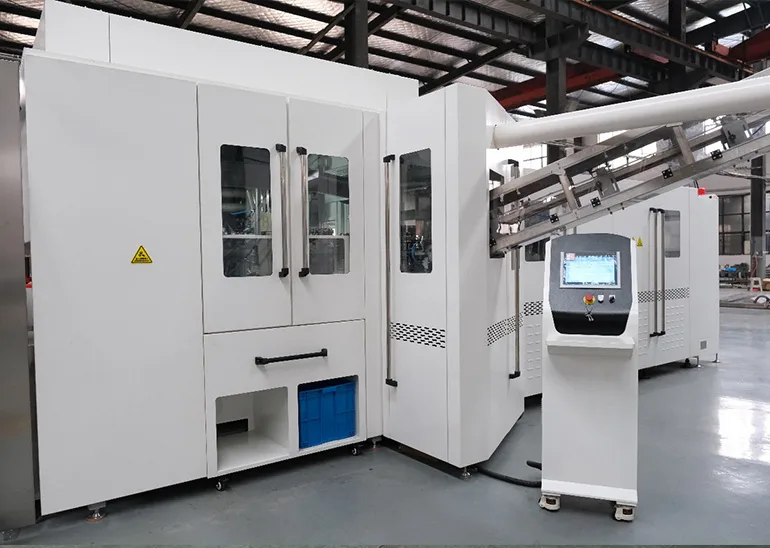
A combiblock joins blow moulding, filling and capping into one frame with one drive and one control system. The preform goes in at one end and the capped bottle comes out at the other, with no intermediate buffer and no bottle storage between blowing and filling.
A conventional line stores empty bottles between the blower and the filler, and that buffer is floor space, conveyor, and a place where bottles collect dust. A combiblock removes all three, and because the three machines share one control system, one operator can run the block. The saving is in the building, not in the machine price.
| Configuration | What is inside | Typical use |
|---|---|---|
| 3-in-1 monoblock | Rinse, fill, cap | Still water in bought bottles |
| Combiblock | Blow, fill, cap | PET lines with in-house blowing |
| Combiblock + labeller | Blow, fill, cap, label | Single-footprint PET line |
| Combiblock + packer | Blow to case | High-volume single-format plant |
Valve count, utility schedule and footprint sit on the Blow-fill-cap Combibloc for Still Water page.
The valve follows the product, not the block. Still water runs gravity or volumetric; oil runs load cell; CSD runs isobaric; juice runs hot fill or volumetric. The block is the frame, and the valve set is specified per product family, which is why one combiblock cannot simply switch between water and CSD.
Throughput and change-part lists are on the Still Water 5L Volumetric page rather than in this note.
Consistent dimensions, a stable colour and a controlled moisture level. A preform that varies in neck dimension stops the filler; one that varies in temperature response changes the bottle. The block cannot compensate for an inconsistent input.
The same question is worked through from another angle in What Are the Advantages of Blowing Filling Capping Machines.
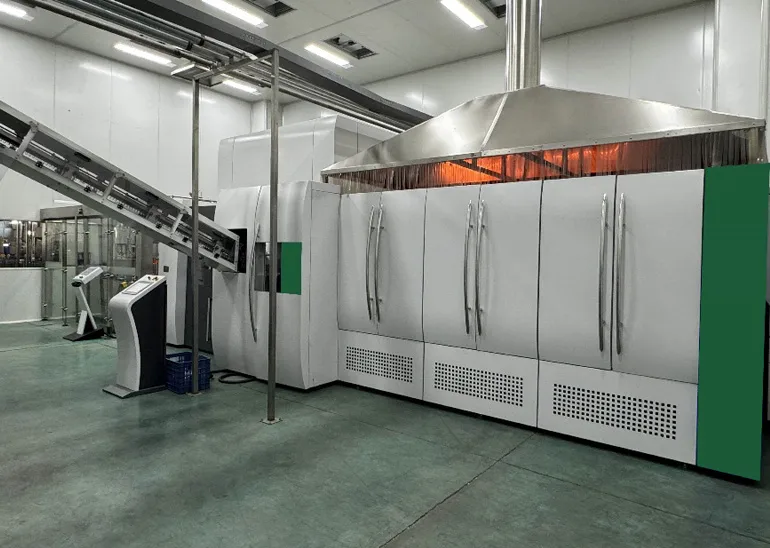
Oven lamp checks, mould cooling water quality and gripper alignment. The oven is the item that drifts quietly: a failing lamp changes the temperature profile and the bottle wall without stopping the machine.
A monoblock combines rinsing, filling and capping. A combiblock adds blow moulding, so the preform goes in and the capped bottle comes out. The two terms are often confused, and the difference is whether a blow moulder is inside the block.
With change parts for the mould, the star wheels and the filling recipe, yes. The changeover is longer than on a filler alone because the mould set changes, and the production factor for a two-format week is lower than for a single format.
The filler stops within seconds because there is no accumulation. That is why the uptime target for a combiblock is set for the block, not for each machine, and why preventive maintenance on the blower is not optional.
It removes the empty-bottle buffer and the conveyor between the blower and the filler, which is the largest space item on a conventional PET line. The exact saving depends on the buffer length in the original layout.
Through a CIP circuit that covers the filler and the product path; the blowing side is cleaned separately as a dry section. The two cleaning regimes run on different schedules and should not be merged in the plan.
Country: Kazakhstan
Product: PET Bottled Carbonated Soft Drinks
Capacity: 12000BPH (1L)
Solution:Carbonated Drinks Production Line
Country: Maldives
Product: PET Bottled Mineralized Water
Capacity: 24,000BPH (500ml); 2 Lines
Solution:Water Production Line



 +86 13921964455
 [email protected]

A2 Dongjiu Industrial Park, 30 East Jintang Road, Tangshi, Zhangjiagang, Jiangsu 215600, China


