
| Valve type | Hot-fill, up to 85 C |
| Capacity | 6,000-36,000 BPH at 0.2-2 L |
| Package | Heat-resistant PET geometry, or glass |
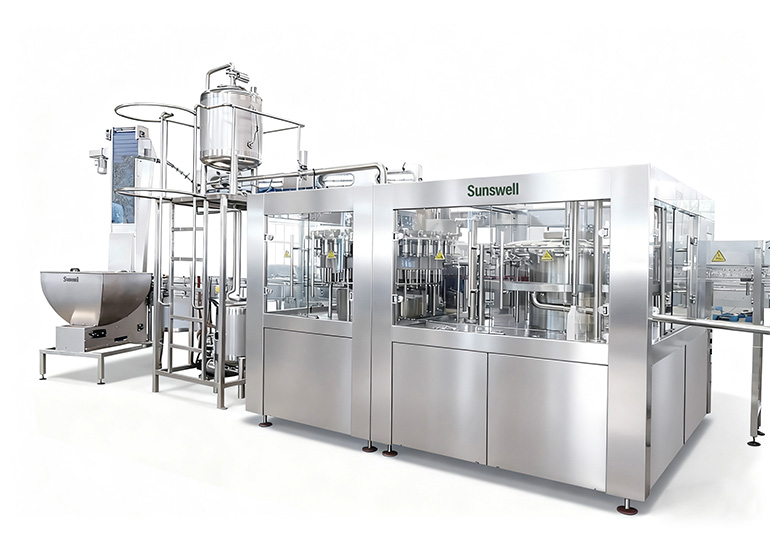
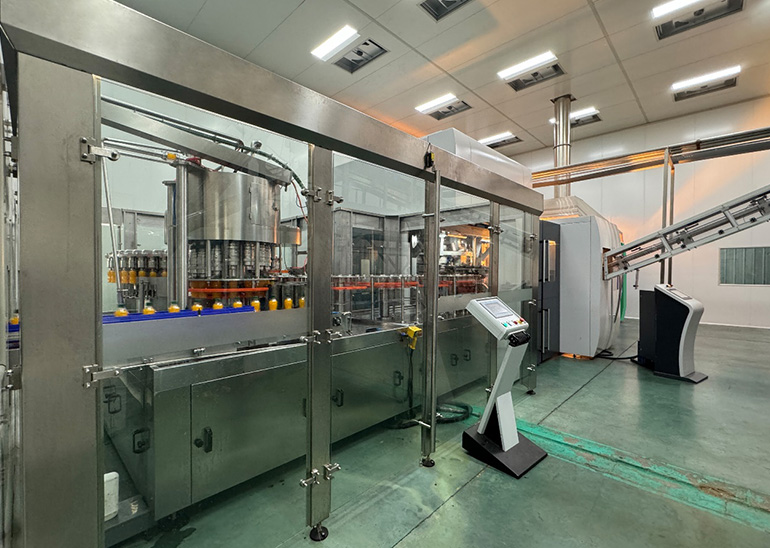
| Line | Hot-fill monobloc with tunnel pasteuriser |
| Products | Juice, tea, nectar, functional drinks |
| Key control | Fill temperature, hold time, cap seal |
Hot filling does two jobs at once: it pasteurises the product on the way to the filler, and the residual heat sanitises the bottle and cap. That is why a hot-fill line can run an acidic juice without a separate bottle steriliser. The price is a heat-resistant bottle and a longer cooling tunnel.
Temperature control is a critical aspect of hotfill processing, directly impacting product safety and shelf life.
Fill temperature and hold time together set the pasteurisation result. Below the target, shelf life is at risk; above it, the product cooks and the bottle deforms. The number belongs to the product and the bottle, not to the machine, and it should be written into the acceptance protocol with a tolerance.
It involves heating the juice to a specific temperature and then filling it into bottles or containers, followed by sealing to maintain freshness.
| Route | Temperature | What it costs |
|---|---|---|
| Hot fill | Up to 85 C | Heat-resistant bottle and a cooling tunnel |
| Cold fill with preservative | Ambient | Formulation constraint, not a machine constraint |
| Cold fill with in-line pasteuriser | Product-side only | Separate pasteuriser and a closed filling zone |
| Hot fill in glass | Up to 85 C | Glass mass, slower line, higher transport cost |
Site requirements, air and water consumption sit with the Hotfill Type Filling Machine for Juice.
Cap seals and filling valve O-rings, because they see the highest temperature every cycle. A seal that is fine on a water line at 20 C will harden in weeks at 85 C. The spare parts list should carry those two items in proportion to the number of valves, not as a single set.
Throughput and change-part lists are on the Juice By Volumetric Filler page rather than in this note.
With a storage trial on the actual product, bottle and closure, held at the intended temperature and sampled on a schedule. Changing the fill temperature, the bottle or the cap invalidates the previous result, which is why those three are treated as one specification.
The same question is worked through from another angle in Key Features to Look for in a Mechanical Hotfill.
Up to 85 C, set per product and per bottle. The exact set point and tolerance belong in the product specification, because acidity, pulp content and bottle wall thickness all move it.
No. Standard PET softens and deforms at fill temperature. The bottle needs a heat-resistant geometry, and the mould and preform are part of the project, not an afterthought.
It depends on the hold tube volume and the heater capacity. The line is not production-ready until the return temperature is stable, so start-up time belongs in the daily plan rather than being discovered at shift start.
Yes, if the filler, the recipe and the downstream cooling are specified for both. Tea usually needs a finer filtration step and a different deaeration setting, so the changeover is a recipe and filter change, not just a new label.
Country: Turkey
Product: Glass and PET Bottled Juice
Capacity: 20000BPH(330ml) Glass Bottle; 4000BPH(3L) PET Bottle
Solution:Juice Production Line
Country:Kazakhstan
Product: PET Bottled Sparkling Water, Canned Soft Drink, Canned Tea
Capacity: 25000CPH (250ml)
Solution:Three Lines,7000BPH(1.5L), 15000CPH(330ml),15000CPH(450ml)



 +86 13921964455
 [email protected]

A2 Dongjiu Industrial Park, 30 East Jintang Road, Tangshi, Zhangjiagang, Jiangsu 215600, China


