
| Filling system | Isobaric for beer and CSD, volumetric for juice and tea |
| Capacity | Up to 25,000 CPH |
| Can sizes | Standard 250, 330 and 500 ml |
| Seaming | Roller seamer integrated with the filler |
| Options | Hot fill for juice and tea, nitrogen dosing |
| Key control | Fill level, seam tightness, dissolved oxygen |
A can line is counted in cans per hour because the container is the unit the seamer closes. CPH and BPH cannot be converted without the fill volume, and the downstream packer is sized in cases per hour. Comparing a 24,000 CPH can line with a 24,000 BPH bottle line compares two different plants.
Compressed air for the seamer and the air conveyor, CO2 for purging, and the tear-down cans used for seam checks every shift. None of these appear in the machine price. A line running 24,000 CPH can consume a measurable share of its operating cost in air alone.
| Product | Filling principle | Critical measurement |
|---|---|---|
| Beer | Isobaric, cold | Dissolved oxygen and seam tightness |
| CSD and soda | Isobaric, cold | CO2 retention and fill height |
| Juice and tea | Volumetric or hot fill | Fill temperature and seam integrity |
| Energy drinks | Isobaric or volumetric | Dissolved oxygen and closure |
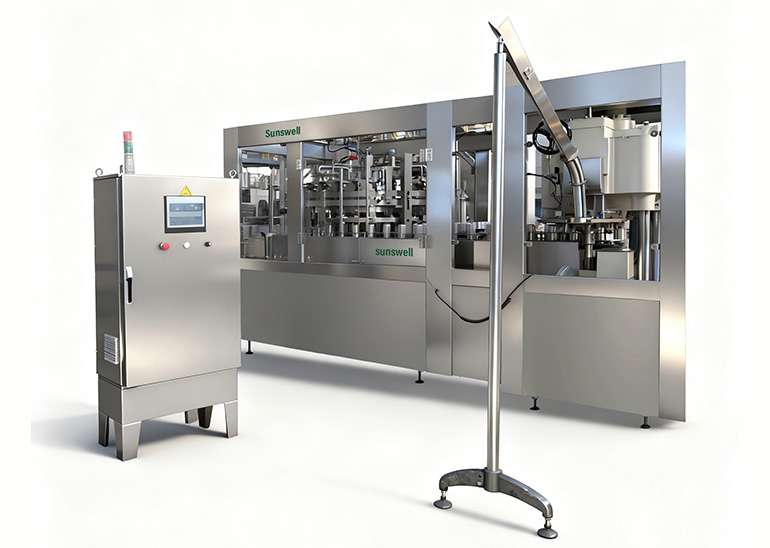
Rated output, change parts and services are listed on the Aluminum Can Filling Machine for Beer, Carbonated Soft Drink page.
A heated product path, a fill temperature control loop and a cooling tunnel after seaming. The can itself tolerates the heat; the lining and the product do not always. The temperature window belongs to the product specification.
Throughput and change-part lists are on the Aluminum Can Filling Machine for Hotfill Juice and Tea page rather than in this note.
Cans are light and rigid, so they move on air conveyors and mass conveyors with low back pressure. Dents come from jams and from accumulation pressure, not from the filler. A can line that dents is a conveyor setting problem before it is a machine problem.
The same question is worked through from another angle in How Aluminum Can Fillers Handle Hotfill Juice.
Yes, with change parts for the filler, the seamer and the conveyor. Changeover time is the real cost. Two formats on one line normally means 40-90 minutes per switch and a lower production factor.
It is common for beer, juice and some CSD, where headspace oxygen has to be pushed down. It is an option with a consumable cost, so it belongs in the utility and consumable schedule, not in the base price.
Usually conveyor pressure or a jam at a transfer, not the can quality. Air conveyor pressure, guide rail gaps and accumulation length are the three settings to check first.
Yes, at the same filler, because the fill volume per cycle is smaller. The seamer and the packer still have to carry the higher can rate, which is why the line rating is set on cans per hour, not litres.
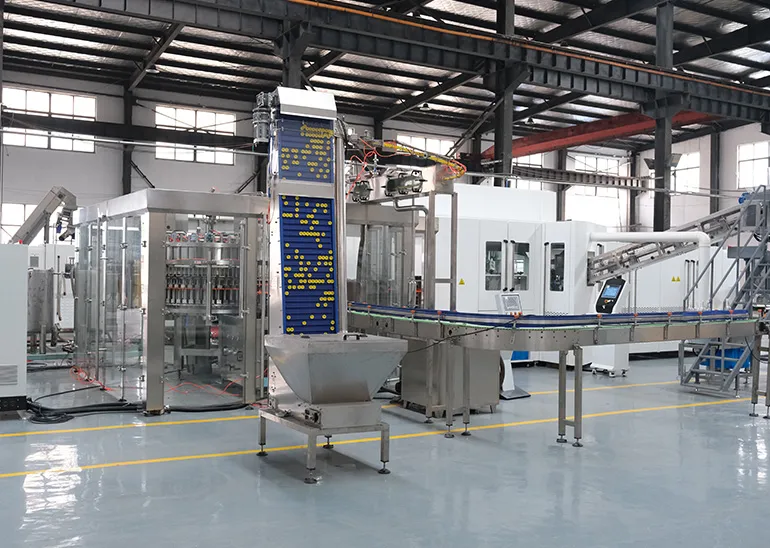
Country: Syria
Product: Aluminum Canned Carbonated Soft Drinks
Capacity: 24000CPH (250ml)
Solution:Carbonated Drinks Production Line
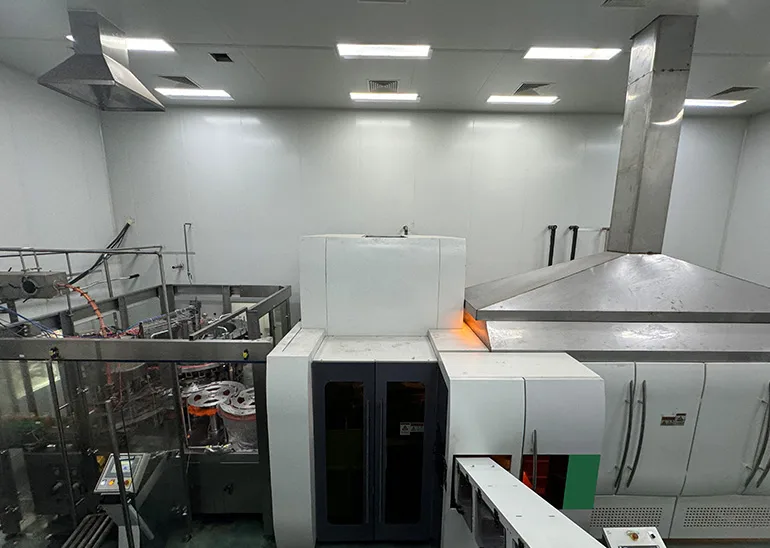
Country:Kazakhstan
Product: PET Bottled Sparkling Water, Canned Soft Drink, Canned Tea
Capacity: 25000CPH (250ml)
Solution:Three Lines,7000BPH(1.5L), 15000CPH(330ml),15000CPH(450ml)



 +86 13921964455
 [email protected]

A2 Dongjiu Industrial Park, 30 East Jintang Road, Tangshi, Zhangjiagang, Jiangsu 215600, China


