
| Types | Shrink wrap, wrap-around carton, carton packing, tray |
| Speed | Matched to the filler; usually the line bottleneck |
| Key control | Film tension, seal temperature, case squareness |
| Contact material | PE film, corrugated board, tray board |
| Key decision | Shrink, carton or tray |
| Line position | After labelling, before palletizing |
Shrink wrap is the cheapest per case and the fastest, and it suits retail where the pack is the display unit. A wrap-around carton gives print area and stack strength for distribution. A tray with shrink is a compromise used where the pack needs both protection and visibility.
From the pack footprint plus the wrap allowance and the tunnel shrinkage. A film that is too narrow leaves the base exposed; too wide and the pack gets a double layer at the seam. Width is a per-format setting, like the lane guides.
| Pack format | Cost per case | What it protects |
|---|---|---|
| Shrink wrap | Lowest | Retail display, short distribution |
| Tray + shrink | Middle | Stacking and visibility |
| Wrap-around carton | Higher | Print area and long distribution |
| Regular slotted carton | Highest board use | Fragile packs and export |
Site requirements, air and power consumption sit with the Wrap-round Film Shrink Wrapping.
Consistent board thickness, a stable score line and a flat stack. A board that varies in caliper jams the magazine and produces wonky cases. The packer is set for one board specification, and a cheaper board is not a saving.
Site requirements, air and power consumption sit with the Carton Packing.
It reaches the pallet, the film width and the truck. A pattern that does not fit the pallet footprint wastes cube, and a pattern that does not match the retail unit costs the customer a repack. Pattern is a commercial decision as much as an engineering one.
The same question is worked through from another angle in How Palletizers Optimize High-Speed Packaging.
It follows the pack weight and the transport distance, and it is set with the film supplier. A thinner film saves cost per pack and fails earlier in a long distribution chain.
It is rated in packs or cases per hour and must exceed the filler output in cases. The limiting factor is normally the tunnel dwell time, not the wrapping speed.
Not without a change of the packing module. Shrink and wrap-around carton are different machines with different board or film paths, so a plant running both normally has two packers.
The pattern that fits the pallet footprint and the retail unit. It is decided with the palletizer and the film width at the same time, because changing it later changes three machines.
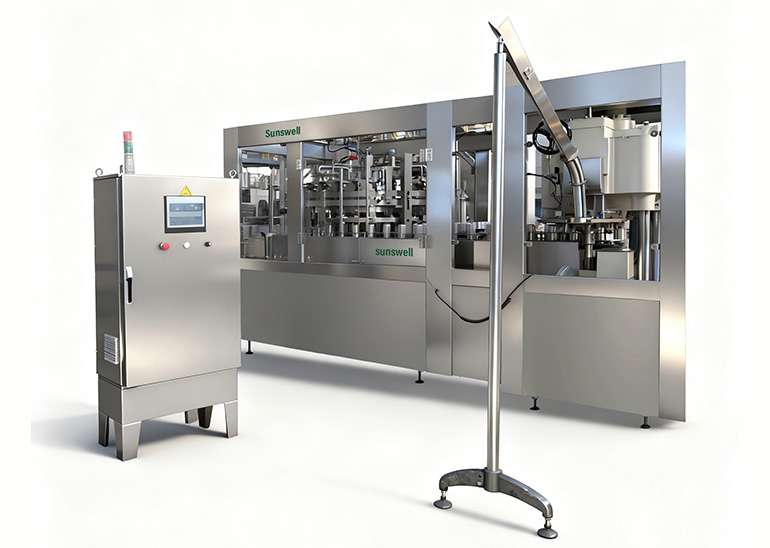
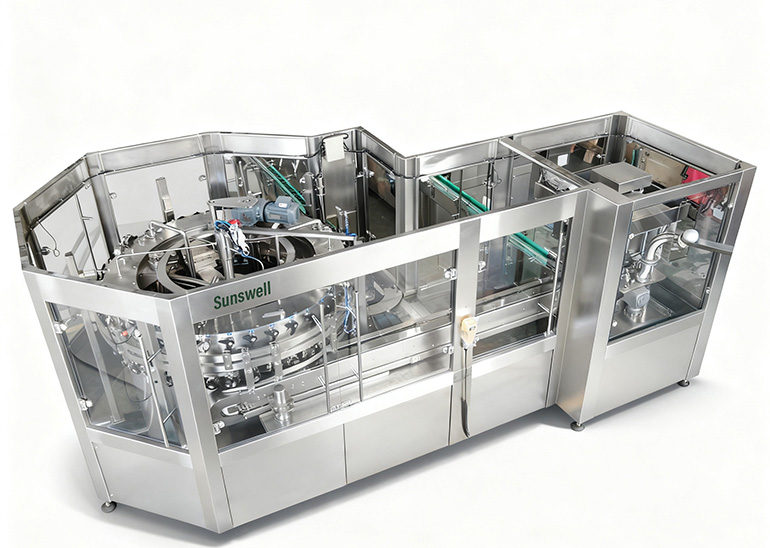
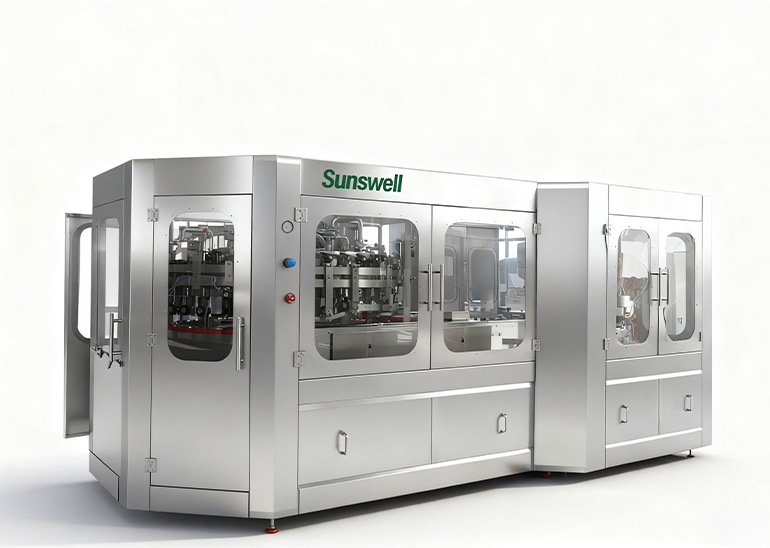
Country:Kazakhstan
Product: PET Bottled Sparkling Water, Canned Soft Drink, Canned Tea
Capacity: 25000CPH (250ml)
Solution:Three Lines,7000BPH(1.5L), 15000CPH(330ml),15000CPH(450ml)



 +86 13921964455
 [email protected]

A2 Dongjiu Industrial Park, 30 East Jintang Road, Tangshi, Zhangjiagang, Jiangsu 215600, China


