
| Types | Shrink wrap, wrap-around carton, carton packing, tray |
| Speed | Matched to the filler; usually the line bottleneck |
| Key control | Film tension, seal temperature, case squareness |
| Wetted parts | PE film, corrugated board, tray board |
| Key decision | Shrink, carton or tray |
| Line position | After labelling, before palletizing |
Shrink wrap is the cheapest per case and the fastest, and it suits retail where the pack is the display unit. A wrap-around carton gives print area and stack strength for distribution. A tray with shrink is a compromise used where the pack needs both protection and visibility.
Film tension and seal temperature. A pack that is tight on the line but loose after cooling has been sealed too cold; a pack with a torn corner has been sealed too hot or cooled too fast. Both show up as returns, not as line stops, which is why they are easy to miss at commissioning.
| Pack format | Cost per case | What it protects |
|---|---|---|
| Shrink wrap | Lowest | Retail display, short distribution |
| Tray + shrink | Middle | Stacking and visibility |
| Wrap-around carton | Higher | Print area and long distribution |
| Regular slotted carton | Highest board use | Fragile packs and export |
Site requirements, air and power consumption sit with the Wrap-round Film Shrink Wrapping.
When the market needs print on the case, when the pack has to stack high in a warehouse, or when the product is sold through distribution rather than direct to retail. A carton costs more per case, and it protects the bottles and carries the brand where shrink film cannot.
Reference unit for this duty: the Carton Packing.
In cases per hour, at the same format, with margin for film changes and seal cooling. A packer rated below the filler sets the line rating, and the shortfall appears as bottles accumulating before the packer rather than as a machine fault.
The same question is worked through from another angle in How to Optimize Palletizers for Efficient Packaging.
It reaches the pallet, the film width and the truck. A pattern that does not fit the pallet footprint wastes cube, and a pattern that does not match the retail unit costs the customer a repack. Pattern is a commercial decision as much as an engineering one.
At 24 bottles per case, 1,000 cases per hour. The packer, the palletizer and the label supply all have to carry that number, and the line rating is the lowest of them.
With different lane guides and a film width change, yes. The changeover is mechanical on a semi-automatic packer, so a plant selling both formats usually accepts a scheduled stop between runs.
It is rated in packs or cases per hour and must exceed the filler output in cases. The limiting factor is normally the tunnel dwell time, not the wrapping speed.
Too much heat, too little tension, or a film that is too thin for the pack weight. A pack that sags after cooling was sealed outside its window.
Not without a change of the packing module. Shrink and wrap-around carton are different machines with different board or film paths, so a plant running both normally has two packers.
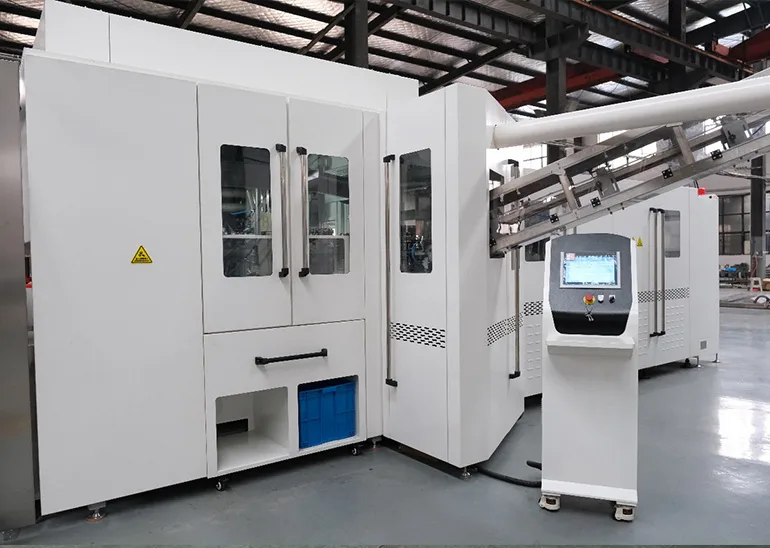
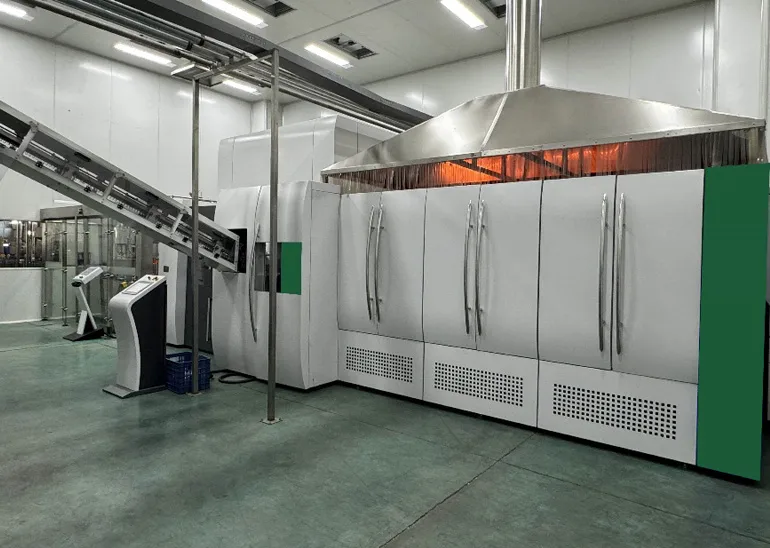
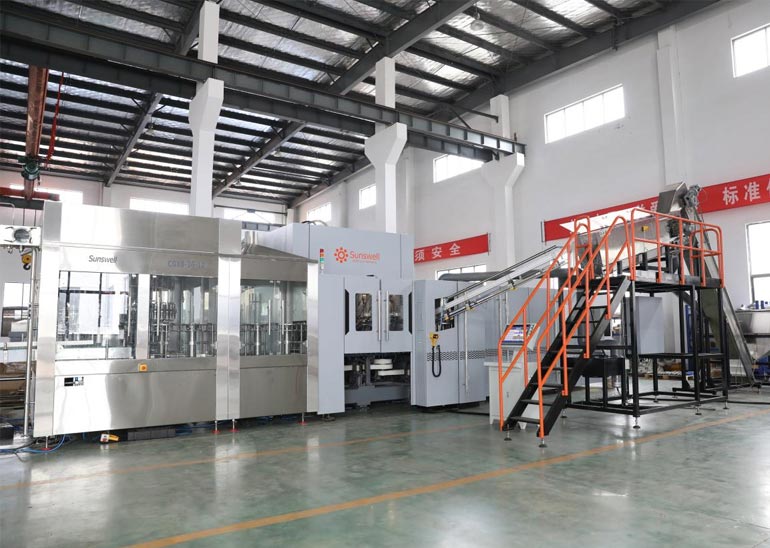
Country:Kazakhstan
Product: PET Bottled Sparkling Water, Canned Soft Drink, Canned Tea
Capacity: 25000CPH (250ml)
Solution:Three Lines,7000BPH(1.5L), 15000CPH(330ml),15000CPH(450ml)



 +86 13921964455
 [email protected]

A2 Dongjiu Industrial Park, 30 East Jintang Road, Tangshi, Zhangjiagang, Jiangsu 215600, China


