| Combines | Blow moulding, filling and capping in one block |
| Rated output | 2,000-48,000 BPH |
| Format range | 0.2-16 L PET |
| Products | Still water, CSD, juice, tea, edible oil |
| Valves | Load cell, volumetric, mechanical or semi-electric |
| Operation | One operator for the complete block |
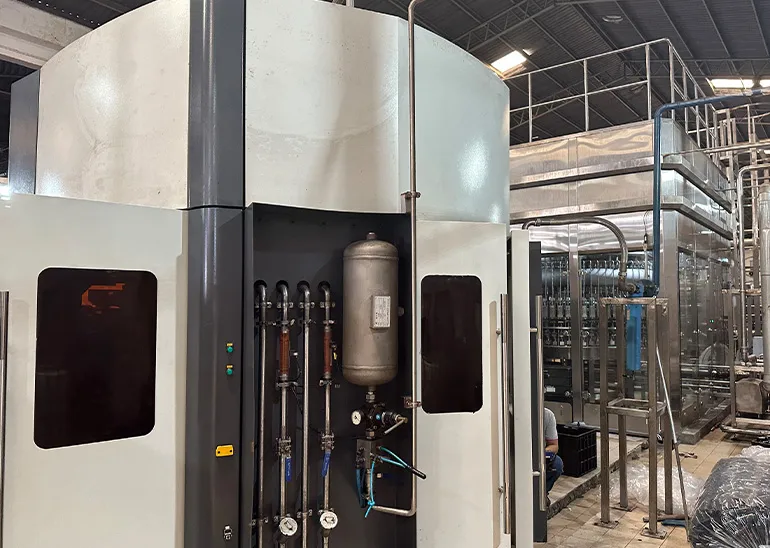
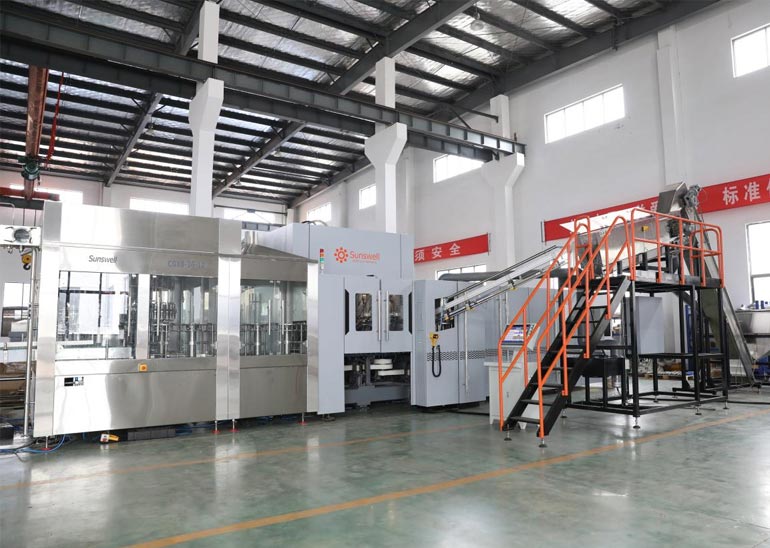
A combiblock joins blow moulding, filling and capping into one frame with one drive and one control system. The preform goes in at one end and the capped bottle comes out at the other, with no intermediate buffer and no bottle storage between blowing and filling.
A conventional line stores empty bottles between the blower and the filler, and that buffer is floor space, conveyor, and a place where bottles collect dust. A combiblock removes all three, and because the three machines share one control system, one operator can run the block. The saving is in the building, not in the machine price.
| Configuration | What is inside | Typical use |
|---|---|---|
| 3-in-1 monoblock | Rinse, fill, cap | Still water in bought bottles |
| Combiblock | Blow, fill, cap | PET lines with in-house blowing |
| Combiblock + labeller | Blow, fill, cap, label | Single-footprint PET line |
| Combiblock + packer | Blow to case | High-volume single-format plant |
Where this becomes a line rather than a single machine, the Blow-fill-cap Combibloc for CSD & Sparkling Water is the starting point.
The valve follows the product, not the block. Still water runs gravity or volumetric; oil runs load cell; CSD runs isobaric; juice runs hot fill or volumetric. The block is the frame, and the valve set is specified per product family, which is why one combiblock cannot simply switch between water and CSD.
Rated output, change parts and services are listed on the Blow-fill-cap Combibloc for Still Water page.
Consistent dimensions, a stable colour and a controlled moisture level. A preform that varies in neck dimension stops the filler; one that varies in temperature response changes the bottle. The block cannot compensate for an inconsistent input.
The same question is worked through from another angle in Comparing Blow-Fill-Cap vs Mechanical Filling for Still Water.
A monoblock combines rinsing, filling and capping. A combiblock adds blow moulding, so the preform goes in and the capped bottle comes out. The two terms are often confused, and the difference is whether a blow moulder is inside the block.
It is designed for one operator on the complete block, which is fewer people than three separate machines need. The saving is real only if the plant also removes the buffer and the bottle handling between stations.
Through a CIP circuit that covers the filler and the product path; the blowing side is cleaned separately as a dry section. The two cleaning regimes run on different schedules and should not be merged in the plan.
It needs high-pressure air for blowing, which is usually a dedicated circuit. Sharing a low-pressure line with the rest of the plant is the most common cause of unstable bottle quality.
Country: Kazakhstan
Product: PET Bottled Carbonated Soft Drinks
Capacity: 12000BPH (1L)
Solution:Carbonated Drinks Production Line
Country: Maldives
Product: PET Bottled Mineralized Water
Capacity: 24,000BPH (500ml); 2 Lines
Solution:Water Production Line



 +86 13921964455
 [email protected]

A2 Dongjiu Industrial Park, 30 East Jintang Road, Tangshi, Zhangjiagang, Jiangsu 215600, China