
| Supply scope | Printers, coders, cap feeders, nitrogen dosers, detectors |
| Function | Support the filler without changing its rating |
| Key control | Position, timing, consumable cost |
| Integration | Signals from the filler PLC or a standalone sensor |
| Key decision | Whether the device earns its cost per 1,000 units |
| Typical position | After the filler, before the packer |
Support equipment does not raise the filler rating. It removes a manual task, a reject source or a compliance risk. The test is simple: if the device stops, does the line stop, and does the defect rate rise? If neither, it is a convenience rather than a control.
Position follows the signal. A coder needs the bottle presented at a fixed gap; a cap feeder needs a buffer before the capper; a detector needs a clear view and a reject gate downstream. Moving any of them changes the timing and the reject logic.
Internal stress of the template is completely relieved, and it is kept at about 500°C for 36 hours in a vacuum state, and gradually cooled out. After the furnace is finished, the template will not be deformed after long-term use.
| Device | What it controls | Consumable |
|---|---|---|
| Coder or printer | Date and batch code | Ink, solvent or laser power |
| Cap feeder | Cap supply to the capper | None, but a buffer is needed |
| Nitrogen doser | Headspace oxygen | Nitrogen per 1,000 units |
| Fill level detector | Reject decision | None, but a reject gate is needed |
Rated output, change parts and services are listed on the Accessory page.
Run the device at the line rating, not at a demonstration speed, and count rejects with the device on and off. Acceptance at half speed hides the timing problem that appears in the first production week.
The unit behind this configuration is the Conveying.
A consistent cap, a correct chute angle and a hopper that is never empty. Most cap jams are the chute and the level, not the sorter. A low-level sensor that stops the line before the hopper empties prevents most of them.
The same question is worked through from another angle in Nitrogen Dosing Machine: Dose, Timing and Dissolved Oxygen.
No. It does not change the filler rating. It reduces headspace oxygen, which protects shelf life. Its value is measured in shelf life and rejects, not in BPH.
A coder applies variable data such as a date or batch code. A labeller applies the product label. Both sit on the conveyor, but only the labeller carries brand and legal product information.
Yes. Detection without a reject gate only records the defect. The gate needs a shift register so it rejects the bottle that was measured, not the one behind it.
Between the filler and the closure, close enough that the gas stays in the headspace. Moving it further downstream wastes gas and gives an unstable result.


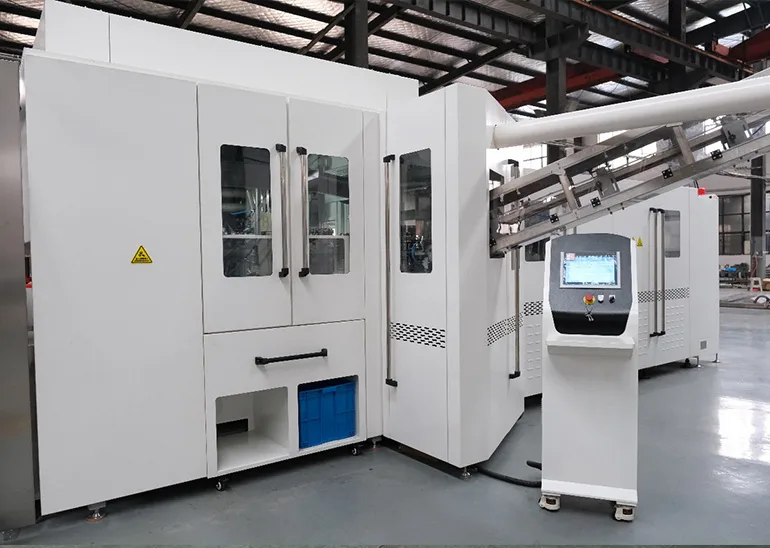
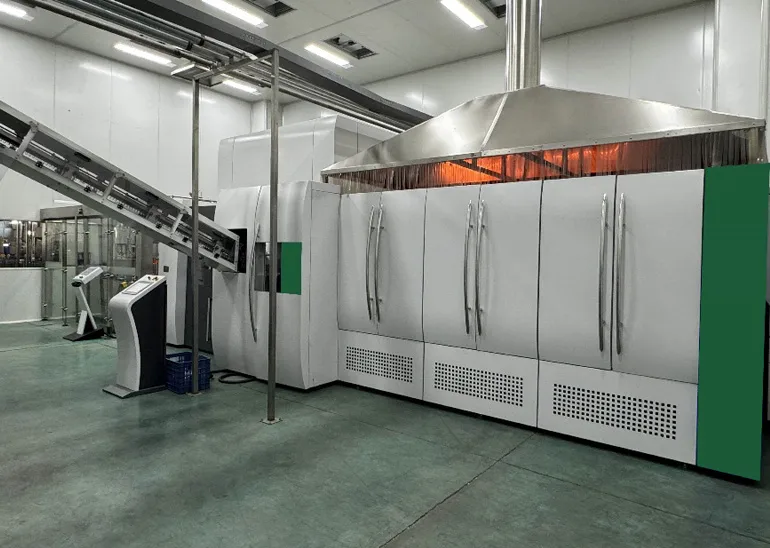
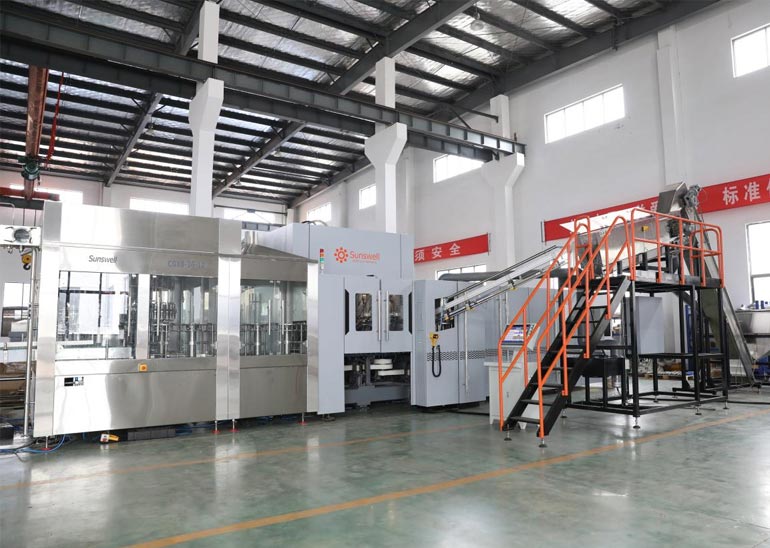
Country:Kazakhstan
Product: PET Bottled Sparkling Water, Canned Soft Drink, Canned Tea
Capacity: 25000CPH (250ml)
Solution:Three Lines,7000BPH(1.5L), 15000CPH(330ml),15000CPH(450ml)


 +86 13921964455
 [email protected]

A2 Dongjiu Industrial Park, 30 East Jintang Road, Tangshi, Zhangjiagang, Jiangsu 215600, China


