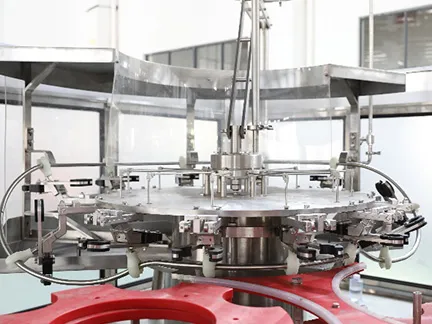
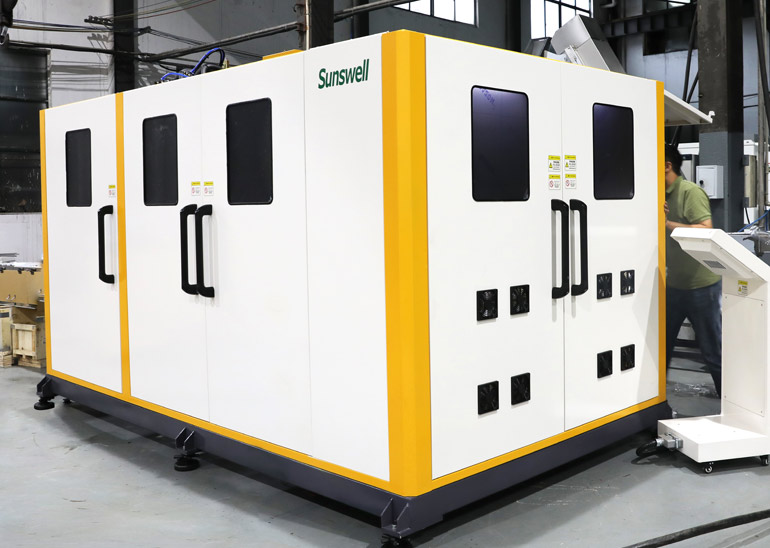
| Types | Linear and rotary blow moulding |
| Input | PET preform, heated in an oven before blowing |
| Output | Bottle matched to the filler neck and format |
| Key control | Preform temperature profile, mould cooling, stretch ratio |
| Integration | Stand-alone, or inside a combiblock |
| Key decision | Blow in-house or buy bottles |
The preform temperature profile decides where the material goes. Too cold and the base is thin; too hot and the wall stretches unevenly. The mould cools the bottle into shape, and the stretch ratio set by the rod and the mould height fixes the wall distribution.
Blowing needs high-pressure air, and producing it is the largest single energy cost in a PET line. Recovery of blowing air, correct nozzle sizing and leak maintenance on the high-pressure circuit are the three measures that move the number, and none of them is visible in a machine quotation.
| Machine | Output pattern | Format changes |
|---|---|---|
| Linear | Lower output, more formats | Frequent, shorter changeover |
| Rotary | High output, fewer formats | Longer changeover, more cavities |
| Two-stage on site | Preform bought in | Mould per format still required |
| Combiblock integrated | Linked to filler | Changeover stops the whole block |
Where this becomes a line rather than a single machine, the Linear Blow Molding is the starting point.
Neck finish decides the filler and capper change parts. Body shape decides the star wheels and guide rails. Wall thickness decides whether the bottle survives the filler and the conveyor. A lightweighting project that changes the base is a filling line project as much as a bottle project.
Throughput and change-part lists are on the Rotary Blow Molding page rather than in this note.
Zone by zone along the preform, with more heat at the body and less at the neck. The profile follows the preform geometry and the bottle design. It is set once and checked on a schedule, because lamp ageing shifts it slowly.
The same question is worked through from another angle in Blow Molding Machines for Custom PET Bottle Production.
Because the neck is the dimension that mates with the cap. It is shielded from the lamps and often cooled directly, so it stays below the point where the material would relax. A warm neck deforms under the capper and leaks.
One preform per bottle. The preform weight is the bottle weight, so preform lightweighting is the main material saving, and it changes the blowing recipe and often the mould.
High-pressure air, typically in the range set by the machine builder for the bottle size. The exact figure and the consumption belong in the utility schedule; it is the largest energy item on a PET line.
Indirectly. Wall thickness distribution and base quality decide the bottle's mechanical strength and its barrier performance. A bottle that passes the drop test can still lose carbonation if the wall is thin at the base.
It is a scheduled stop measured in tens of minutes on a linear machine and longer on a rotary machine, because every cavity is set. The oven recipe and the stretch rod height change with the mould.
It can, with an adjusted temperature profile, because recycled resin melts and stretches differently. The change is a process change, and it should be validated on the actual resin before production.
Country: Maldives
Product: PET Bottled Mineralized Water
Capacity: 24,000BPH (500ml); 2 Lines
Solution:Water Production Line
Country:Kazakhstan
Product: PET Bottled Sparkling Water, Canned Soft Drink, Canned Tea
Capacity: 25000CPH (250ml)
Solution:Three Lines,7000BPH(1.5L), 15000CPH(330ml),15000CPH(450ml)



 +86 13921964455
 [email protected]

A2 Dongjiu Industrial Park, 30 East Jintang Road, Tangshi, Zhangjiagang, Jiangsu 215600, China