
| Filling principle | Hot-fill, up to 85 C |
| Rated output | 6,000-36,000 BPH at 0.2-2 L |
| Package | Heat-resistant PET geometry, or glass |
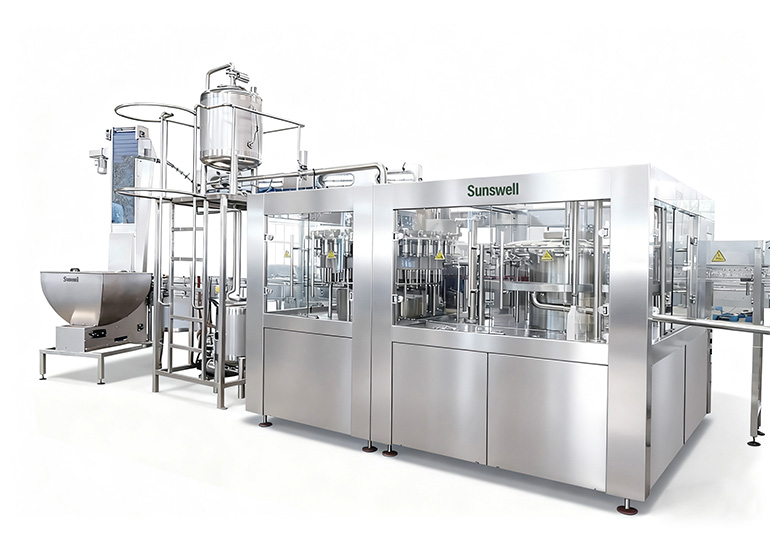
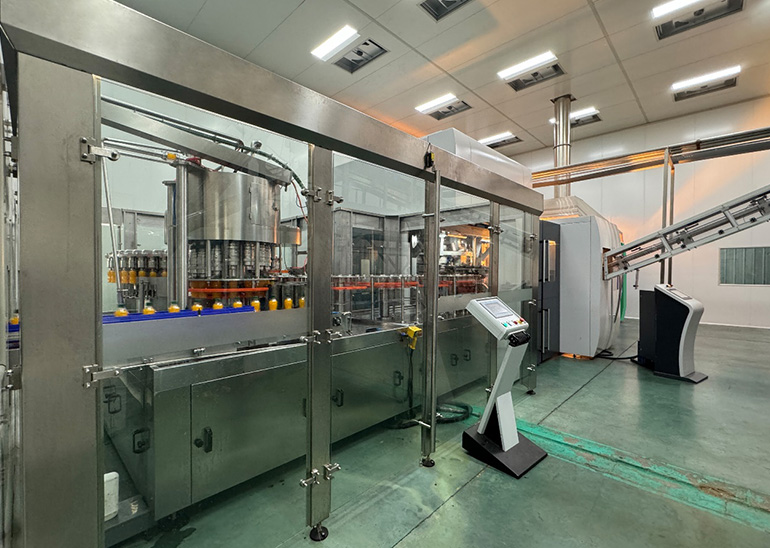
| Line | Hot-fill monobloc with tunnel pasteuriser |
| Products | Juice, tea, nectar, functional drinks |
| Key control | Fill temperature, hold time, cap seal |
Hot filling does two jobs at once: it pasteurises the product on the way to the filler, and the residual heat sanitises the bottle and cap. That is why a hot-fill line can run an acidic juice without a separate bottle steriliser. The price is a heat-resistant bottle and a longer cooling tunnel.
Select bottles with appropriate material properties and thickness to withstand the temperature differentials experienced during the hotfill and cooling stages.
Fill temperature and hold time together set the pasteurisation result. Below the target, shelf life is at risk; above it, the product cooks and the bottle deforms. The number belongs to the product and the bottle, not to the machine, and it should be written into the acceptance protocol with a tolerance.
Implement automated temperature control systems to adjust heating and cooling parameters in real-time and minimize temperature fluctuations.
| Route | Temperature | What it costs |
|---|---|---|
| Hot fill | Up to 85 C | Heat-resistant bottle and a cooling tunnel |
| Cold fill with preservative | Ambient | Formulation constraint, not a machine constraint |
| Cold fill with in-line pasteuriser | Product-side only | Separate pasteuriser and a closed filling zone |
| Hot fill in glass | Up to 85 C | Glass mass, slower line, higher transport cost |
The unit behind this configuration is the Hotfill Type Filling Machine for Juice.
Pulp needs either a larger valve bore or a piston filler, and it needs continuous gentle agitation in the bowl. Dead corners in the product path settle fibre, then release it as a slug into the next bottle. Bowl geometry and return-flow design matter more than valve count here.
Common causes of foaming include inadequate temperature control, improper handling of fruit pulp, and excessive aeration during the filling process.
Sizing for this duty runs through the Juice By Volumetric Filler, where the valve count is set out.
Compare them on the product, not on the machine. Hot fill suits acidic juice and tea in heat-resistant PET. Cold fill needs a preservative system or a separate sanitising step, but it protects heat-sensitive flavours and vitamins and uses a lighter bottle. The decision is a product decision with a packaging cost attached.
The same question is worked through from another angle in How to Reduce Downtime in Hotfill Juice Lines.
No. Standard PET softens and deforms at fill temperature. The bottle needs a heat-resistant geometry, and the mould and preform are part of the project, not an afterthought.
It depends on the hold tube volume and the heater capacity. The line is not production-ready until the return temperature is stable, so start-up time belongs in the daily plan rather than being discovered at shift start.
Yes, if the filler, the recipe and the downstream cooling are specified for both. Tea usually needs a finer filtration step and a different deaeration setting, so the changeover is a recipe and filter change, not just a new label.
A controlled ramp rather than a cold plunge, so the bottle does not deform under vacuum. The tunnel zones are set per bottle geometry and validated with a temperature probe in the product.
Country: Turkey
Product: Glass and PET Bottled Juice
Capacity: 20000BPH(330ml) Glass Bottle; 4000BPH(3L) PET Bottle
Solution:Juice Production Line
Country:Kazakhstan
Product: PET Bottled Sparkling Water, Canned Soft Drink, Canned Tea
Capacity: 25000CPH (250ml)
Solution:Three Lines,7000BPH(1.5L), 15000CPH(330ml),15000CPH(450ml)



 +86 13921964455
 [email protected]

A2 Dongjiu Industrial Park, 30 East Jintang Road, Tangshi, Zhangjiagang, Jiangsu 215600, China


