| Scope | Filling, capping, labelling and packing equipment |
| Sizing basis | Demand in units per day, divided by productive hours and a production factor |
| Production factor | 0.65-0.85 depending on formats and changeovers |
| Key control | Fill accuracy, closure integrity, changeover time |
| Key decision | One flexible line or two dedicated lines |
| Acceptance | Output, accuracy, closure and changeover, measured |
Four inputs fix the shortlist: the product, the package, the daily demand and the number of formats per week. Everything else, including the brand of the PLC, is a detail that can be settled after those four are written down.
By considering factors such as viscosity handling, flow rate, pressure requirements, and product compatibility, you can make an informed choice that meets your operational needs.
Compare the lowest rated station, the changeover time, the CIP time and the consumable cost per 1,000 units. A lower price with a slower packer or a longer CIP is not a lower cost. Ask both suppliers for the same four numbers in writing.
| Decision | What it fixes | What it does not fix |
|---|---|---|
| Filling principle | Product and accuracy | Downstream capacity |
| Valve count | Rated BPH | Changeover and CIP time |
| Automation level | Labour per shift | Product quality |
| Line layout | Floor space and flow | Throughput of the slowest station |
Site requirements, air and water consumption sit with the Gravity Filling Machine for Still Water.
When the formats are far apart, or when one product cannot tolerate the cleaning regime of the other. A single flexible line carries changeover cost every day; two dedicated lines carry capital cost once. The crossover is usually visible in the annual changeover hours.
Where this becomes a line rather than a single machine, the Volumetric Filling Machine for Still Water is the starting point.
It proves the machine meets the written specification on the agreed product, at the agreed format, in the builder workshop. It does not prove the line will run in your building. Both tests are needed, and the second one is where most disputes start.
The same question is worked through from another angle in ISO 22000 Food Safety Management for Beverage Bottling Plants.
Bottles per day divided by productive hours, then divided by a production factor of 0.65-0.85. The factor covers changeover, cleaning and downstream stops. Sizing at 1.0 is the most common planning error.
BPH is bottles per hour; divide by 60 for bottles per minute. A 12,000 BPH line runs at 200 bottles per minute, and every downstream machine has to carry that rate.
Capacity is usually added by a second line or by a downstream upgrade, not by speeding up the filler. The filler, the capper and the packer are matched, so raising one alone moves the bottleneck.
Between 0.65 and 0.85. A single-format line on one shift sits near 0.85; a line with four formats and two changeovers per shift sits near 0.65.
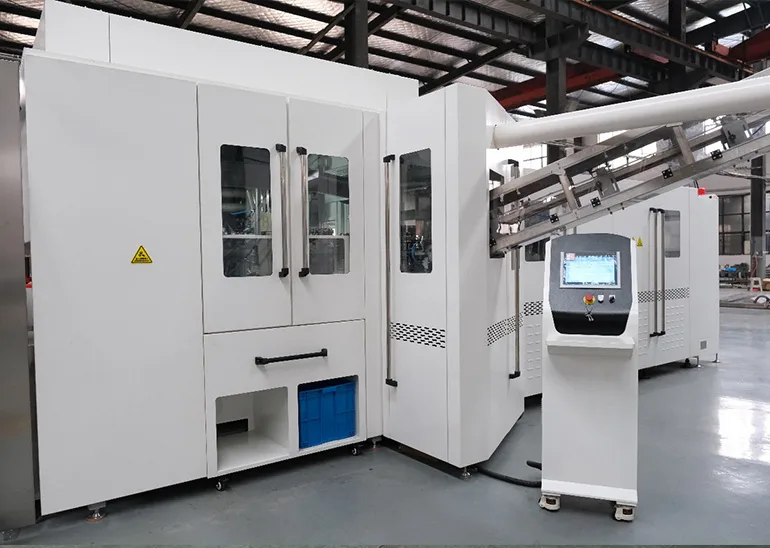
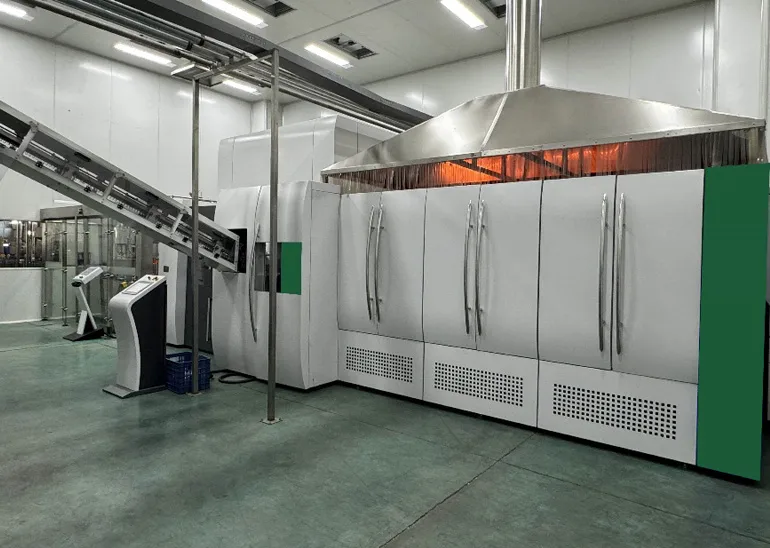
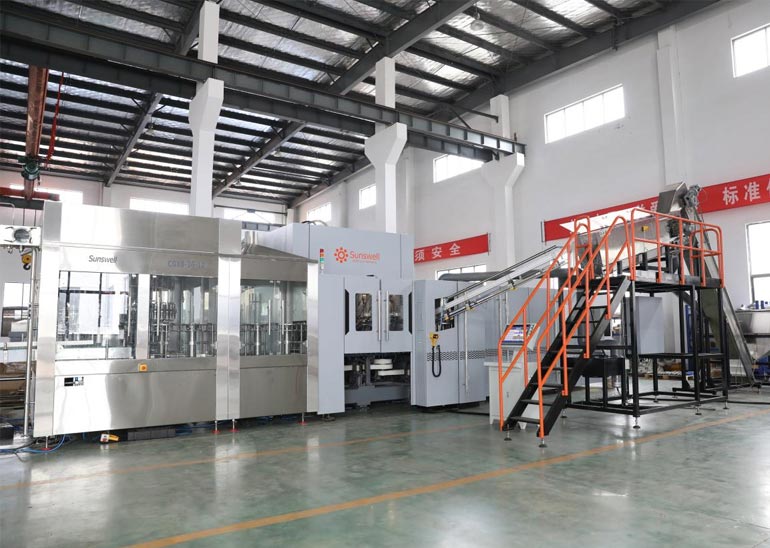
Country:Kazakhstan
Product: PET Bottled Sparkling Water, Canned Soft Drink, Canned Tea
Capacity: 25000CPH (250ml)
Solution:Three Lines,7000BPH(1.5L), 15000CPH(330ml),15000CPH(450ml)



 +86 13921964455
 [email protected]

A2 Dongjiu Industrial Park, 30 East Jintang Road, Tangshi, Zhangjiagang, Jiangsu 215600, China